
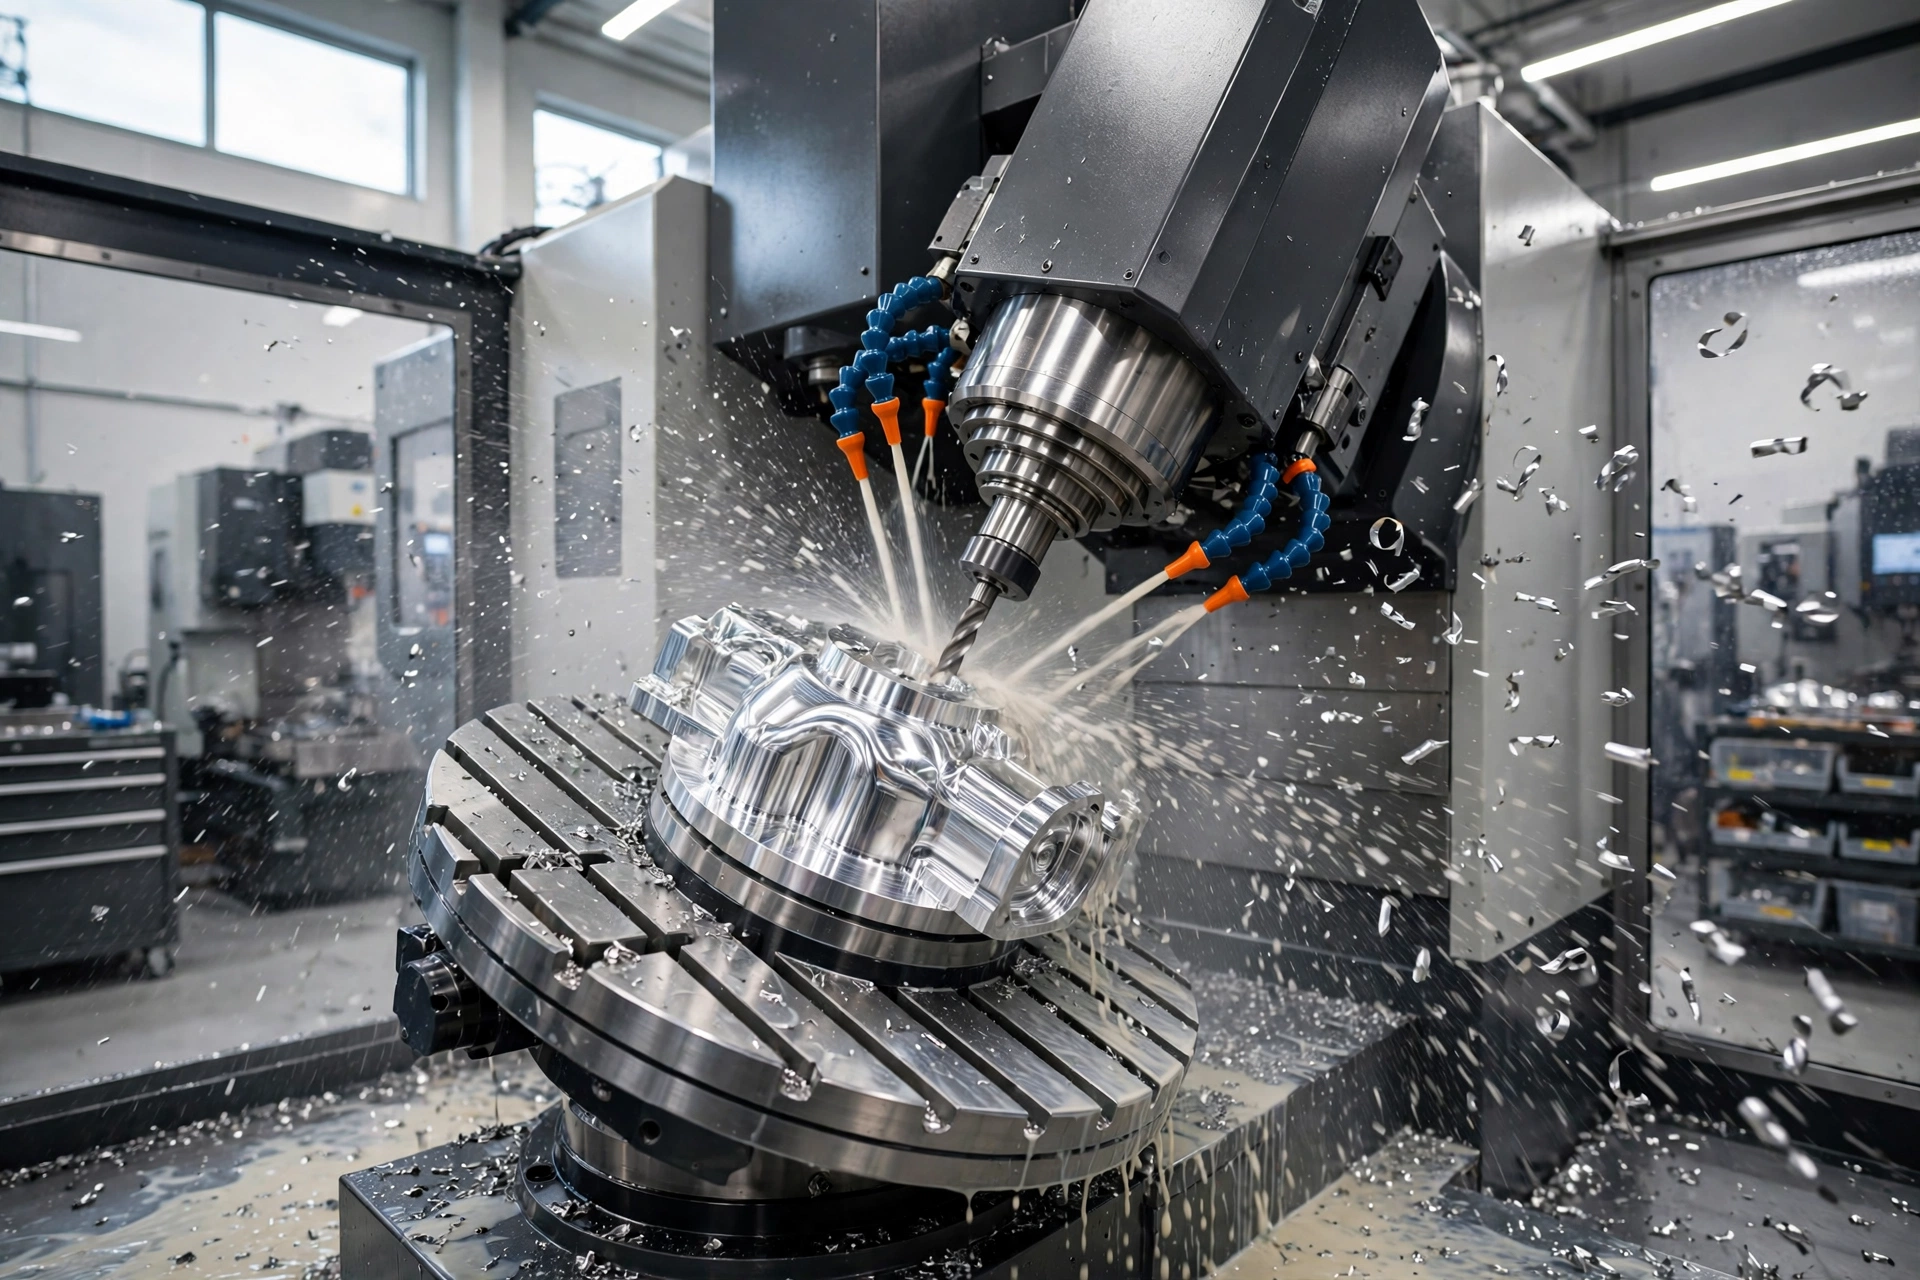
CNC machining cost is driven by five main factors: machine time, material, part complexity, tolerance and surface finish, and order volume. Machine time is the single largest cost, since a part that takes longer to cut ties up an expensive machine and a skilled operator for longer. The most reliable way to lower cost is to simplify the part and loosen tolerances wherever the function allows, rather than to shop for a cheaper hourly rate.
Material and tolerance compound that: hard-to-machine metals and tight tolerances both slow the process down. Two quotes for the same drawing with the same tolerances and finish from competent shops are usually within a reasonable range of each other, because they’re pricing the same physics.
The five main CNC cost drivers
Every CNC quote comes down to the same core variables:
- Machine time: how long the part takes to cut, including roughing and finishing passes. This is usually the biggest line item; it’s a function of material removal rate, not just part size.
- Material: the raw stock cost plus how easily the material machines, since both feed into the final price independently of each other.
- Complexity: deep pockets, thin walls, tight internal corners, and features that need special tooling or multiple setups.
- Tolerance and finish: how precise the critical dimensions are and how smooth the surface must be.
- Volume: how the fixed costs of setup and programming spread across the run.
The reason two quotes for the “same” part can differ is that these factors interact. A small tolerance change on one feature can force slower passes and extra inspection, which raises machine time and cost across the board — it rarely stays contained to just that one dimension.
What’s actually inside a CNC quote
A machining quote isn’t a single number pulled from a price list; it’s a build-up of several distinct cost categories, even though the supplier usually presents it as one line per part.
- Raw material cost (stock plus any waste factor)
- Programming and CAM time to generate the tool paths
- Setup time to build or select workholding and dial in the first part
- Machine cycle time per part
- Secondary operations like deburring, tapping, or finishing
- Inspection time scaled to the tolerance and quantity of critical features
Understanding this breakdown is useful because it tells you where a design change actually saves money — shortening cycle time helps on every unit, while reducing setup complexity mostly helps on small runs where setup cost isn’t yet amortized across many parts.
How material choice affects cost
Material affects price in two ways: the stock cost and the machinability. Aluminum (such as 6061) is inexpensive and cuts quickly, while stainless steel costs more in both material and machine time because it work-hardens and wears tools faster. Titanium and superalloys are expensive on both counts: costly raw stock and slow cutting speeds. Plastics are usually cheaper to machine than metals but are less rigid, so thin features can deflect.
A practical move is to confirm the material early. If a part does not strictly need titanium, specifying aluminum or stainless can cut cost substantially without compromising function. The tolerances achievable across these materials are wide: standard CNC operations hold around ±0.001″, and precision processes can reach far tighter, but pushing precision adds cost in every material.
How tolerance and finish affect cost
Tolerance
Tolerance is one of the most expensive things to over-specify. A general machined feature is forgiving, but a tight tolerance on a bearing fit or sealing surface requires slower finishing passes, better tooling, temperature control, and more inspection.
Calling out a tight tolerance on every dimension, when only one or two features need it, quietly inflates the whole quote — every toleranced feature on a drawing typically needs to be measured and recorded, not just the ones that matter functionally, unless the drawing makes clear which dimensions are critical and which are reference only.
Surface finish
Surface finish works the same way. A standard as-machined finish is included; a fine finish, bead blast, anodize, plating, or polish each add steps and cost, both for the finishing operation itself and for the extra handling and packaging needed to protect a cosmetic surface through shipping.
Specify the finish the part actually needs, and only on the surfaces that need it — a finish call-out that applies to the entire part when only the visible face actually matters is a common and avoidable cost adder.
How volume changes the price per part
CNC machining has high fixed costs up front: programming, fixturing, and the first setup. Those costs are spread across the whole run, so the price per part drops as volume rises. This is why a single prototype can cost a surprising amount per piece while the same part at 200 units is far cheaper each.
| Volume | What dominates the price |
|---|---|
| 1 to 10 parts (prototype) | Setup, programming, and fixturing per part are high |
| 10 to 100 parts (low volume) | Fixed costs start to amortize, price per part falls |
| 100+ parts (production) | Machine time per part dominates; unit price stabilizes |
If you expect to scale, tell the shop your projected volumes so they can plan fixturing and quote the production price — a shop that knows a part is headed to 5,000 units can justify investing in a dedicated fixture that wouldn’t make sense for a 5-piece order, and that investment lowers the per-part price at volume even though it raises the cost of the very first batch.
Setup, programming, and fixturing
Before a chip is cut, an engineer programs the tool paths and the team builds or selects workholding to hold the part securely. Complex parts that need multiple setups, where the part is repositioned to reach different faces, cost more because each setup adds time and a chance for misalignment.
Designing a part so it can be machined in fewer setups, or on a 5-axis machine that reaches multiple faces at once, lowers this cost — though 5-axis machine time itself typically carries a higher hourly rate than 3-axis, so the savings only materialize if the setup reduction outweighs that rate difference, which it usually does on genuinely complex geometry.
Hidden cost drivers people often miss
Beyond the headline factors, a few less obvious things routinely move a quote:
- Thin walls and deep, narrow pockets that force slower feed rates to avoid chatter or tool deflection.
- Tight internal corners that require a smaller tool and therefore more passes than a generous radius would.
- Parts that need a specific grain direction or come from a certified material lot, which limits which stock the shop can pull from.
- Last-minute revisions after a quote is locked, which can force re-programming and re-fixturing that a simple “make this hole bigger” request doesn’t obviously suggest.
None of these are exotic — they’re common, and flagging them during a design-for-manufacturing review before the drawing is finalized is far cheaper than discovering them after parts are already in production.
Practical ways to reduce CNC machining cost
These design and sourcing choices reliably lower the number. Here is how to reduce CNC machining cost at the drawing stage:
- Loosen non-critical tolerances. Reserve tight tolerances for features that truly need them; use a standard tolerance for everything else.
- Simplify geometry. Avoid unnecessarily deep pockets, thin walls, and sharp internal corners that need extra tooling or time.
- Choose a machinable material. Use aluminum or a free-machining grade where function allows, instead of a hard-to-machine alloy.
- Reduce setups. Design for fewer orientations, or specify multi-axis machining for complex geometry, to cut setup time.
- Right-size the finish. Only specify premium finishes where appearance or function demands them, and only on the surfaces that need it.
- Batch your order. Combine quantities to spread fixed setup and programming costs across more pieces.
- Get DFM feedback early. A design-for-manufacturing review can flag expensive features before you commit to them.
How to compare CNC quotes fairly
Compare total landed cost, not just the per-part price. Make sure every supplier is quoting the same tolerance, the same finish, and the same inspection scope, and include shipping, any duties, and the expected cost of rework. A quote that looks cheap but omits inspection or assumes looser tolerances is not actually comparable — it’s a different deliverable wearing the same part number.
It’s also worth asking what each quote assumes about your projected volume — a supplier pricing for a one-time order lands on different numbers than one pricing a recurring program. If you are weighing machining against molding, see our CNC machining vs injection molding break-even guide. At XY Machining, we provide DFM feedback with every quote so you can see which features drive your cost and adjust before committing.
Frequently asked questions
How much does CNC machining cost?
There is no flat rate, because cost depends on machine time, material, complexity, tolerance, finish, and volume. The biggest driver is usually how long the part takes to cut. Prototypes cost more per part than production runs because setup and programming are spread across fewer pieces.
Why is CNC machining so expensive for one part?
A single part still carries the full fixed cost of programming, fixturing, and setup, with nothing to spread it across. A prototype also typically needs more inspection and iteration than a production part, which adds cost per piece.
What is the biggest factor in CNC machining cost?
Machine time is usually the largest factor, since it ties up an expensive machine and a skilled operator. Material choice and tolerance are the next biggest levers, because both directly change how long a part takes to cut and inspect.
How can I reduce my CNC machining cost?
Loosen non-critical tolerances, simplify geometry, choose a machinable material, design for fewer setups, right-size the surface finish, batch your order, and get DFM feedback before finalizing the design.
Does material choice really change the price that much?
Yes. Aluminum is cheap and fast to machine, while titanium and superalloys are expensive to buy and slow to cut. Switching to a more machinable material is often the single biggest cost reduction available if the part’s function allows it.
What’s included in a typical CNC machining quote?
A quote typically reflects raw material cost, programming and CAM time, setup and fixturing, machine cycle time per part, secondary operations, finishing and packaging, and margin. It may not include shipping, duties, or inspection unless the supplier states it, so check what is included before comparing quotes.
How much does CNC machining cost per hour?
There is no single hourly rate — it depends on the machine, the material, and the volume. A 3-axis mill costs less per hour than a 5-axis machine, and titanium costs more than aluminum on both material and machine time. Ask for a cost breakdown (material, machine time, setup, and finishing) in your quote so you can see the rate behind the number.
How to calculate CNC machining cost?
Add the material cost to the machining time multiplied by the machine’s hourly rate, then add setup, programming, and finishing costs. The quote breakdown section above shows which lines go into the total — ask your shop for the same breakdown so you can see exactly where the number comes from.


