
What are the different injection molding gate types used in plastic manufacturing? How does injection molding gate design affect part quality, strength, appearance, and production efficiency? Where should an injection molding gate location be placed for the best results?
The selection of the correct injection molding gate type plays an important role in producing high-quality plastic parts. Gate design and placement control how molten plastic enters the mold cavity, affecting filling balance, surface finish, warpage, strength, and overall product performance.
Injection molding gates are small openings that connect the runner system to the mold cavity. Manufacturers carefully select gate designs based on part geometry, material properties, production volume, and appearance requirements. Choosing the right gate helps reduce defects and improves manufacturing consistency.
For businesses requiring professional plastic component production, injection molding services provide advanced manufacturing solutions with optimized mold designs and production processes.
What Is an Injection Molding Gate?
An injection molding gate is the controlled entry point where melted plastic flows from the runner system into the mold cavity. Although it is a small feature in the mold design, it has a major impact on the final quality of the molded part.
During injection molding, molten plastic travels through the nozzle, runner, and gate before filling the cavity. The gate controls the speed, direction, and pressure of material flow.
A properly designed gate helps achieve:
- Balanced cavity filling
- Reduced air traps
- Better surface appearance
- Improved mechanical performance
- Easier part removal
The wrong gate selection can create issues such as weld lines, sink marks, short shots, excessive stress, and visible gate marks.
Why Injection Molding Gate Design Matters
Injection molding gate design is not only about allowing plastic to enter the mold. Engineers consider multiple factors to ensure the material flows correctly and produces consistent parts.
The design process considers:
| 设计因素 | Effect on Molded Parts |
| Gate Size | Controls filling speed and pressure |
| Gate Location | Influences appearance and strength |
| Gate Shape | Affects flow pattern and finishing quality |
| Gate Type | Determines suitability for different applications |
Professional mold designers analyze these factors during the development stage. Companies often combine mold optimization with rapid prototyping services to test product designs before full-scale production.
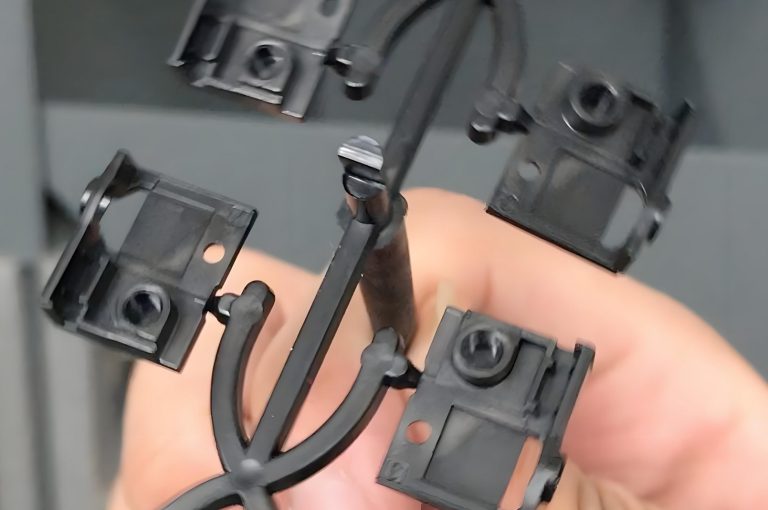
Common Types of Injection Molding Gates
Different applications require different gate designs. The most suitable choice depends on the part shape, material, production requirements, and finishing expectations.
Edge Gate
The edge gate is one of the most commonly used injection molding gates. It is placed along the edge or parting line of the mold.
This gate design provides simple filling control and is suitable for flat or medium-sized components. It is commonly used for consumer products, housings, panels, and general plastic parts.
Advantages of edge gates include:
- Simple mold construction
- Easy processing
- Good filling control
- Suitable for many materials
However, edge gates usually leave a visible gate mark that may require trimming after production.
Tab Gate
A tab gate is a modified version of an edge gate that uses an additional tab area connected to the part.
The purpose of this design is to reduce stress concentration near the gate area. After molding, the tab is removed during finishing.
Tab gates are often used for parts where appearance and stress reduction are important.
Pin Gate
A pin gate is a small circular gate commonly used in three-plate molds. It automatically separates from the molded part when the mold opens.
This design creates a smaller gate mark compared with larger gate types.
Pin gates are suitable for:
- Small precision components
- Cosmetic parts
- Multi-cavity molds
Their compact size allows better control of material flow in detailed parts.
Submarine Gate
A submarine gate, also known as a tunnel gate, enters the mold cavity from below the parting line.
The main advantage of this design is automatic gate separation during ejection. This reduces manual trimming requirements and improves production efficiency.
Submarine gates are commonly used for high-volume manufacturing where automation is important.
Hot Runner Gate
Hot runner gates use heated channels to deliver molten plastic directly into the mold cavity.
Unlike traditional cold runner systems, hot runner systems reduce material waste because the runner material does not solidify after each cycle.
They are commonly used for:
- Large production volumes
- Complex parts
- Multi-cavity molds
Hot runner systems require higher initial investment but can improve long-term production efficiency.
Direct Gate
A direct gate connects the injection nozzle directly to the mold cavity.
This design provides strong material flow and is often used for large components that require high filling pressure.
The disadvantage is that it usually creates a larger gate mark, making it less suitable for visible surfaces.
How to Select the Right Injection Molding Gate Type?
Choosing between different types of injection molding gates requires understanding the product requirements and manufacturing goals.
Engineers evaluate:
- Part size and geometry
- Plastic material characteristics
- Required surface finish
- 生产数量
- Gate removal requirements
- Strength requirements
For example, a cosmetic electronic housing may require a hidden gate location to maintain appearance, while an industrial bracket may prioritize strength and efficient filling.
Manufacturers also consider the expected production environment. High-volume automotive parts often require automated gate solutions, while prototype components may use simpler gate designs.
Injection Molding Gate Location Considerations
该 injection molding gate location directly affects how plastic flows inside the cavity. Incorrect placement can create uneven filling, weak areas, and visible defects.
Common placement guidelines include:
Place Gates Near Thick Sections
Plastic flows more easily through thicker areas. Positioning the gate near thicker sections helps prevent incomplete filling and improves material distribution.
Avoid Visible Surface Areas
For consumer products, manufacturers often place gates on hidden surfaces to maintain appearance.
Consider Flow Direction
The gate should allow smooth material movement throughout the cavity. Poor flow direction can create weld lines or trapped air.
Maintain Balanced Filling
For multi-cavity molds, gate locations should support equal filling across all cavities.
Injection Molding Gate Types Comparison
| Gate Type | 最佳应用 | 主要优势 |
| Edge Gate | General plastic parts | Simple and cost-effective |
| Pin Gate | Precision components | Small gate marks |
| Submarine Gate | Automated production | Automatic separation |
| Hot Runner Gate | High-volume manufacturing | Reduced material waste |
| Direct Gate | Large components | Strong material flow |
Common Injection Molding Gate Problems
Even with proper mold design, incorrect gate selection can create manufacturing problems.
Short Shots
A short shot occurs when molten plastic does not completely fill the mold cavity. This may happen because the gate size is too small or material flow is restricted.
Weld Lines
Weld lines appear when two plastic flow paths meet. They can weaken the part and affect appearance.
Sink Marks
Sink marks occur when cooling shrinkage creates visible depressions. Proper gate placement and cooling design help reduce this issue.
Excessive Gate Marks
Large or poorly positioned gates may leave visible marks that require additional finishing.
Working with experienced manufacturers helps identify these issues early through proper simulation, testing, and production validation.
Role of Mold Design in Gate Selection
Gate selection is closely connected with overall mold design. Engineers must consider cavity layout, cooling channels, material behavior, and production requirements.
A successful mold design balances:
- Manufacturing cost
- Part quality
- 周期时间
- Maintenance requirements
Businesses developing complex products often combine 数控加工服务 with injection molding to create accurate prototypes, tooling components, and production parts.
结语
理解 注塑成型 gate types helps manufacturers create better plastic parts with improved quality, appearance, and performance. The right gate design, placement, and manufacturing method can significantly reduce defects while improving production efficiency.
Every molded component has unique requirements, so engineers must evaluate material properties, part geometry, production volume, and finishing expectations before selecting a gate solution.
By choosing the correct injection molding gate design and optimizing the injection molding gate location, manufacturers can achieve reliable results for prototypes, consumer products, industrial components, and large-scale production applications.
常见问题解答
What are the most common injection molding gate types?
The most common gate types include edge gates, pin gates, submarine gates, hot runner gates, tab gates, and direct gates. Each design provides different benefits depending on part requirements, material, and production volume.
How does injection molding gate location affect part quality?
Gate location controls plastic flow direction, pressure distribution, and cooling behavior. A properly selected location reduces defects and improves strength, appearance, and consistency.
Which injection molding gate is best for high-volume production?
Hot runner and submarine gates are often preferred for high-volume manufacturing because they reduce waste and support automated production. The best choice depends on part design and material.
Why is injection molding gate design important?
Gate design affects filling performance, surface quality, production efficiency, and defect prevention. Proper design ensures the plastic flows evenly throughout the mold cavity.
Can injection molding gates be removed after production?
Yes, many gates can be trimmed or automatically separated depending on the gate type. Some designs, such as submarine and pin gates, simplify gate removal during production.
关于作者 陈帕特里克——XY Machining 应用工程师 帕特里克负责审查XY Machining公司美国工程团队设计的薄壁零件,并与车间人员合作,针对夹具和刀具路径进行优化,以确保精密零件的尺寸公差符合要求。为了在报价前对薄壁零件进行压力测试,, 将您的模型发送给我们的团队.


