
快速回答
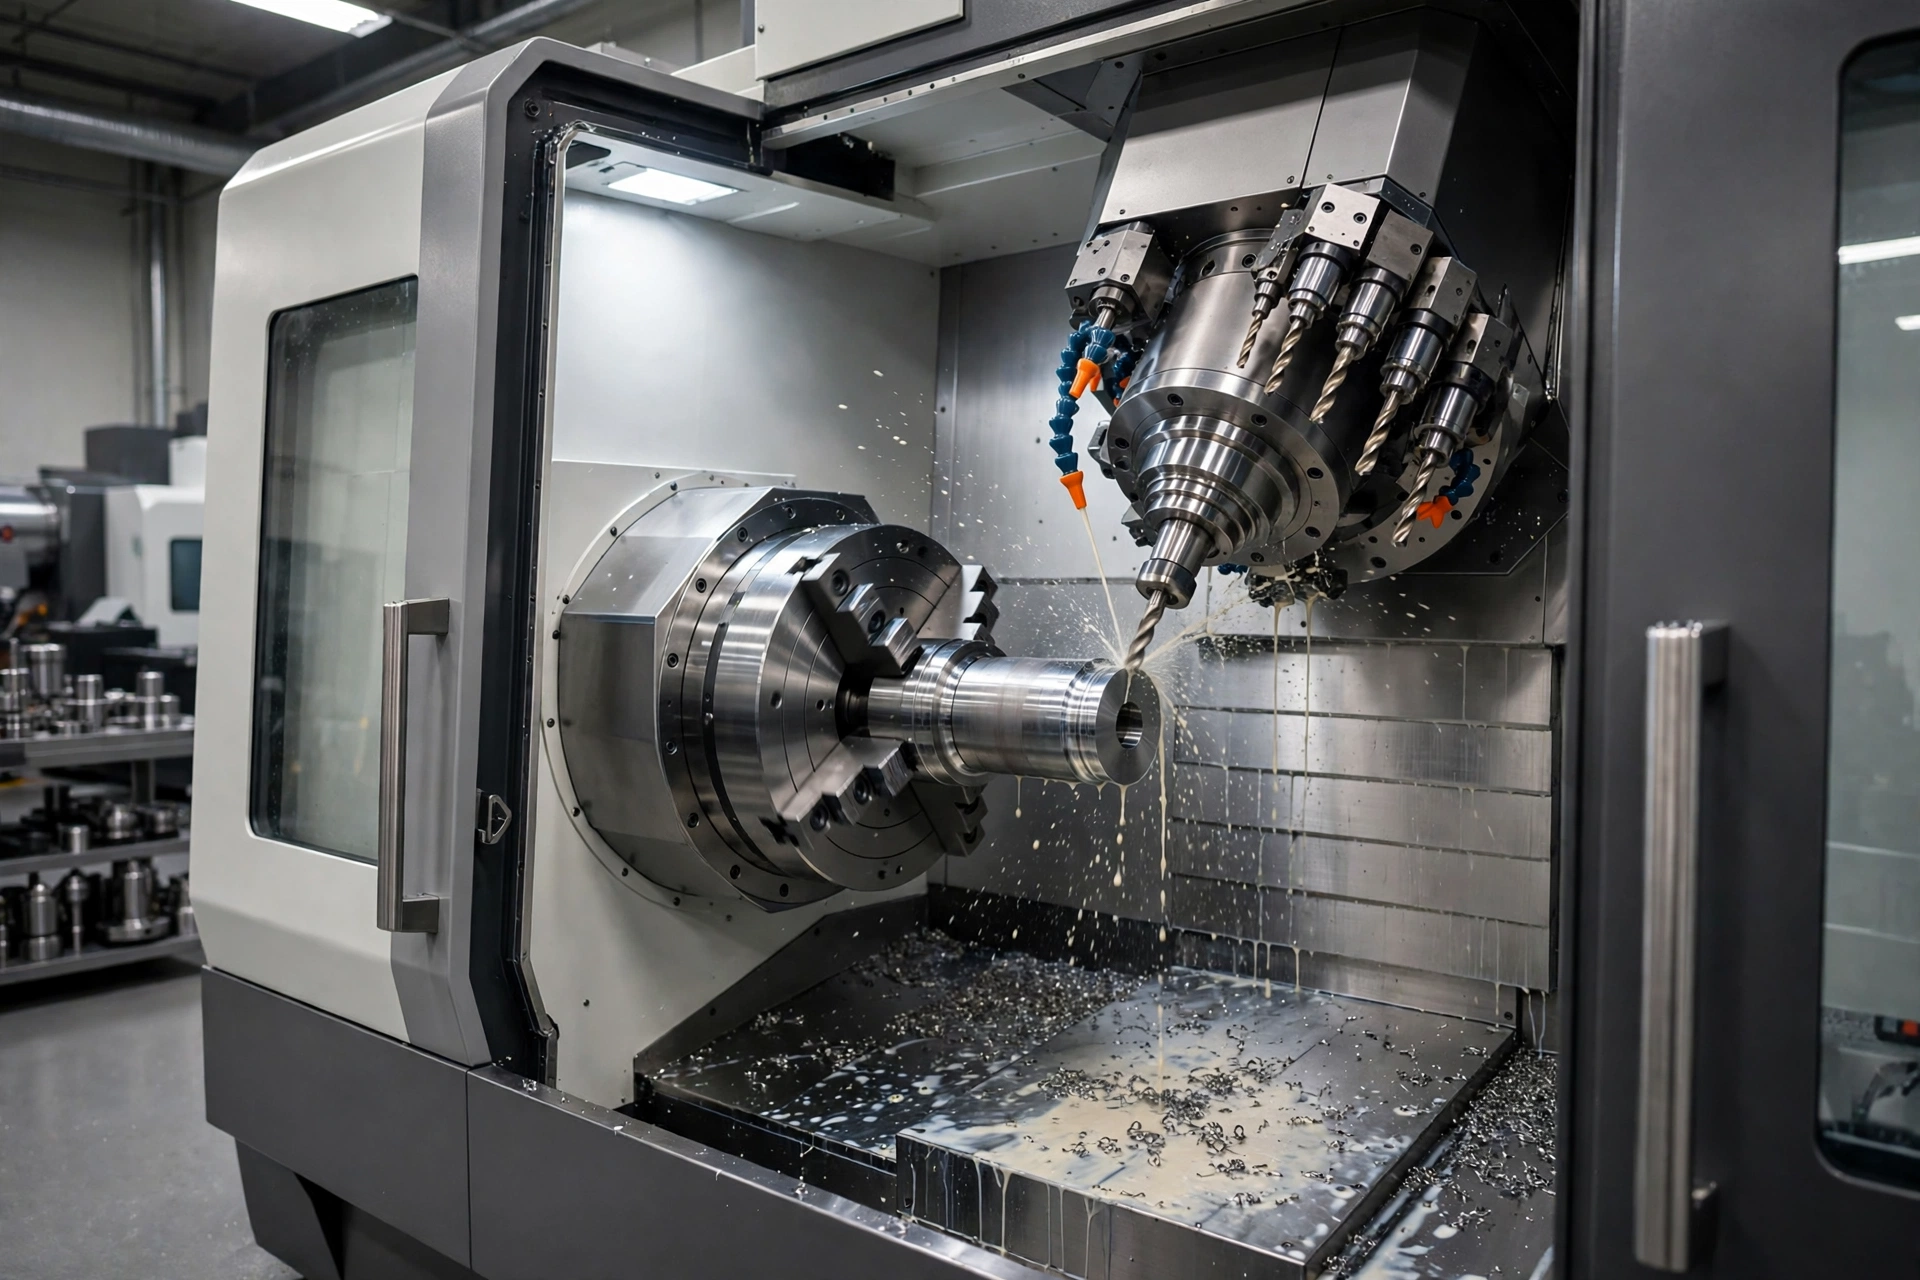
简答: 数控车削 spins the workpiece against a stationary cutting tool to make round features fast, while CNC milling holds the part still and spins the tool to cut flats, slots, pockets, and holes. Most real parts need both.
Running them on a single mill-turn machine — instead of moving the part between two separate machines — removes a second setup, protects your tolerances, and typically shaves days off the lead time. That combination is why most precision shops quote milling and turning as one integrated capability rather than two line items.
A bracket that failed inspection
I still remember the first bracket I sent out that needed a turned boss on one face and a milled slot on the other. We machined the turning on a lathe, walked the part across the shop, re-fixtured it on a mill, and lost the concentricity between the two features by four thousandths of an inch. The part failed inspection.
A mill-turn machine would have held both features in one clamping. That lesson is the whole reason this article exists.
车削与铣削:核心区别
The split is about what moves. In turning, the part rotates and the tool stays put. In milling, the tool rotates and the part stays put (or moves along programmed axes). That single distinction drives everything else — the shapes you can make, the finishes you get, and the cost per part.
| 因子 | 数控车削 | 数控铣削 |
|---|---|---|
| 什么在旋转 | 工件 | 切削工具 |
| 最适合 | 圆柱形、圆形、对称零件 | 平面、槽口、凹槽、复杂的3D结构 |
| 典型部件 | 轴、衬套、销、螺纹螺柱 | 支架、外壳、板、歧管 |
| 环形特征的速度 | 非常快 | 慢 |
| 棱柱状特征上的速度 | 差 | 非常快 |
| 公共轴 | 2轴(X、Z),加带动力刀具 | 3轴,最多5轴 |
| 外径表面光洁度 | 极佳,如镜一般 | 良好,可能会有工具痕迹 |
如果您想更深入地了解两者的对比,我们将在关于……的指南中进行更详细的分析。 数控车削与铣削的对比. 简而言之:它们并非竞争对手。它们是同一份工作的两个部分。.
Why “milling and turning” is searched as one phrase
People type turning and milling or cnc milling and turning together for a reason. Very few functional components are purely round or purely prismatic. A hydraulic fitting is turned on the outside but needs cross-drilled ports milled into it. A motor shaft is turned to diameter but needs a milled keyway.
When you ask a shop for “milling and turning,” you are really asking a practical question: can you finish my whole part without shipping it somewhere else? That is where mill-turn machining earns its keep.
铣车两用机床的实际功能是什么
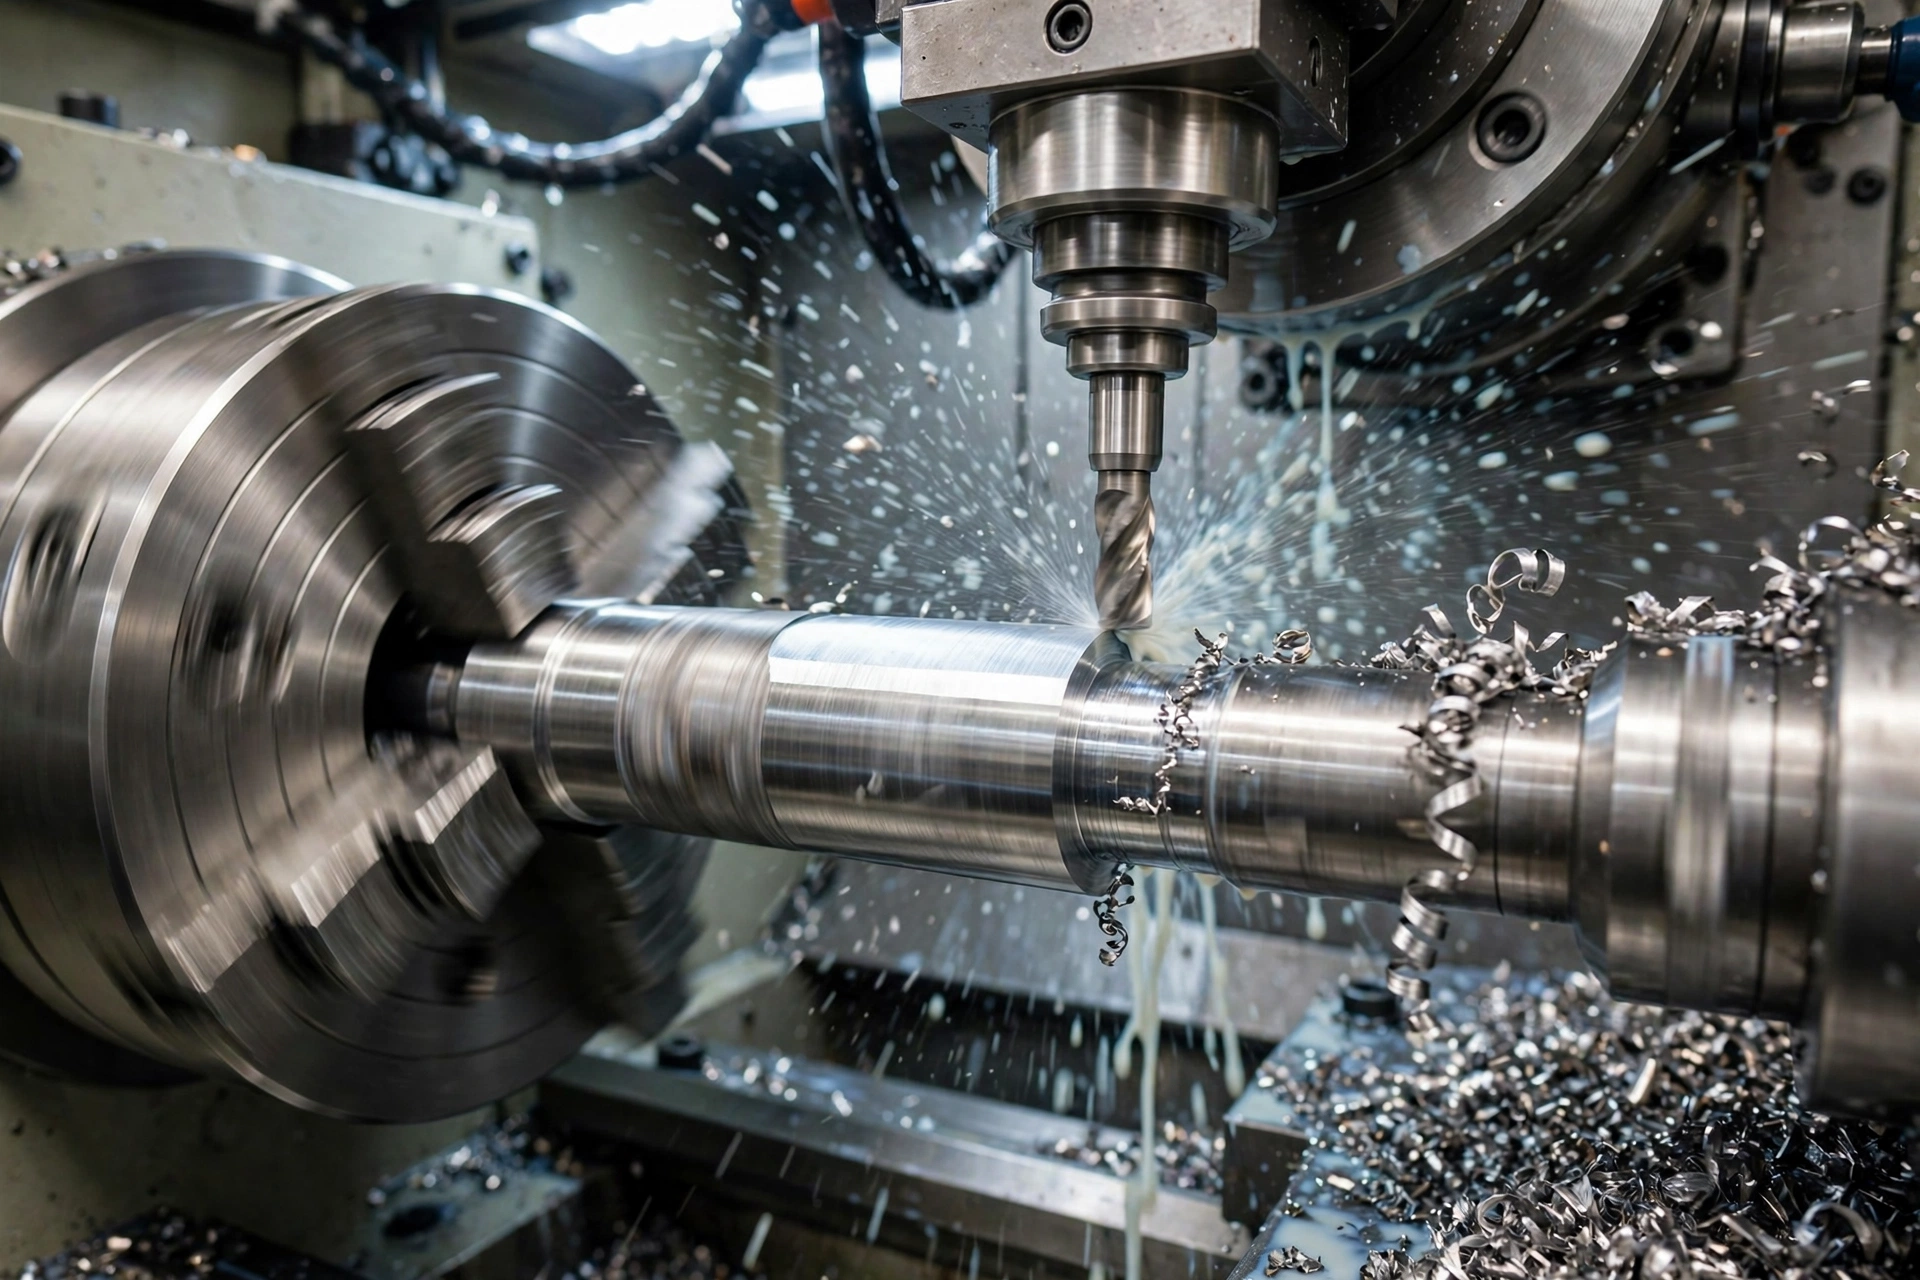
车铣复合中心是一种配备动力铣头且通常带有第二主轴的车床。 工件在车削加工过程中旋转,随后机床停止主轴转动,将工件分度至精确角度,并驱动主轴上的旋转刀具进行平面铣削、偏心钻孔或切削键槽——所有这些操作均无需松开工件夹具。.
这些好处很快就会显现出来:
- One setup, one datum. Every feature is cut relative to the same reference, so concentricity and position error stay tiny.
- No re-fixturing labor. Moving a part between machines is human time, and human time is where cost and mistakes live.
- Shorter lead time. Fewer setups means fewer queue steps between machines.
- Better repeatability at volume. Once the program is proven, part 1 and part 5,000 look identical.
对于一家精密车削供应商而言,这正是根据同一张图纸报价时,3天工期与7天工期之间的区别。.
一项切合实际的成本与交货期对比
Below is a representative comparison for a medium-complexity part — say, a threaded aluminum housing with a turned body and four milled side ports — at a quantity of 250. Numbers are illustrative and vary by geometry, material, and shop, but the shape of the difference is consistent with what we see on the floor.
| 方法 | 设置 | 预计交货期 | 单件相对成本 | 同心度风险 |
|---|---|---|---|---|
| 独立车床 + 独立铣床 | 2(重新安排) | 6–8天 | 基线 (100%) | 更高 |
| 车铣复合加工(单台机床) | 1 | 3–4天 | ~80–90% | 非常低 |
| 仅车削(部分经过重新设计以避免铣削) | 1 | 2–3天 | ~70% | 不适用 |
最后这一点往往被采购人员忽略:有时,最经济的方案就是进行微小的设计调整。 如果某个铣削特征仅仅是因为原始设计师默认采用了它,那么与加工车间简单沟通一下,就能将一个需要两道工序的零件改造成只需一道工序的零件。这正是能够降低单件成本的“面向制造的设计”思维。我们将在 如何降低数控加工成本.
当你仍然希望使用两台独立的机器时
车铣复合加工并不总是最佳选择。在以下情况下,专用机床更具优势:
- Volumes are very high and geometry is simple. A plain turned pin at 100,000 pieces runs cheapest on a fast, dedicated lathe.
- Milling work is heavy and 5-axis. A complex impeller belongs on a full 5轴加工 中心,而不是带铣削头的车床。.
- The turned and milled features have loose tolerances between them. If nothing needs to be concentric, the re-fixturing risk disappears and cost rules the decision.
一家好的加工厂会根据你的图纸推荐合适的加工方案,而不是硬把每个订单都塞到同一台机器上加工。.
材料:铣削与车削的行为有何不同
Material choice changes how each process performs. Free-machining brass and aluminum turn beautifully and mill cleanly. Stainless and titanium turn well but work-harden if the milling feeds are wrong, which is where an experienced operator matters more than the machine’s spec sheet.
| 材料 | 转弯行为 | 铣削行为 | 注释 |
|---|---|---|---|
| 6061铝合金 | 非常棒 | 非常棒 | 原型的默认值;参见 6061 与 7075 |
| 黄铜 C360 | 杰出 | 非常好 | 最易加工的材料 |
| 303/304不锈钢 | 好 | 中等 | 303型机器比304型机器容易得多 |
| 钛 Ti-6Al-4V | 中等 | 苛刻的 | 低进给、锋利的刀具、大量切削液 |
| 德尔林/乙缩醛 | 非常棒 | 非常棒 | 非常适合车削加工的绝缘部件 |
如何向加工厂交代车铣复合加工任务
为了获得准确、快速的报价,请向店家提供:
- A STEP file plus a 2D drawing that calls out the critical dimensions — not every dimension, just the ones that matter for fit and function.
- Tolerances only where you need them. A blanket ±0.001 in on a whole part triples the price for no reason.
- Material and finish clearly stated, including any 阳极氧化 或电镀。.
- Quantity and target date, so the shop can pick the right machine strategy.
这份包含四项内容的简报,是你能够掌控成本和交货周期方面最重要的手段。.
常见问题
数控车削比数控铣削更便宜吗?
For round features, yes — turning removes material far faster than milling because the whole part is spinning. But comparing them in isolation misses the point. The real cost driver is how many setups your part needs. A part that is 90% round and 10% milled is cheapest on a mill-turn machine, because you pay for one setup instead of two. Judge cost by the finished part, not by the individual process.
车铣复合机床与带动力刀具的车床有什么区别?
这两个概念存在重叠,且术语使用较为宽松。配备动力刀具的车床可在工件被夹紧时驱动几个旋转刀具,用于轻型铣削和横向钻孔。 全功能车铣复合中心的功能更为全面,通常会增加Y轴、用于背部加工的第二主轴,以及足够的铣削能力,使得该机床几乎可以视为车床与加工中心的融合体。对于需要一次装夹即可加工的复杂工件,全功能车铣复合中心正是您的理想选择。.
一台机床真的能在车削和铣削加工特征上同时保持公差吗?
是的,这正是买家选择它的原因。由于工件始终固定在卡盘上,因此每个铣削孔和铣削平面都以同一个车削基准为参照。 在第二台机床上重新装夹时可能产生的同心度和真实位置误差,在这里根本不会出现。对于任何需要铣削特征与车削孔保持同心的工件,单次装夹加工都是最可靠的选择。.
我是否需要专门为车铣复合加工来设计我的零件?
虽然不是在初期,但进行一次简短的设计审查还是很有价值的。 尽早将模型发送给加工车间,并询问是否有任何特征会导致额外工序。一些微小的改动——例如调整孔位、放宽非关键公差、增加倒角——就能将一个需要两个工序的零件简化为一个工序即可完成的零件。这一简短的沟通所节省的成本,往往比任何材料替换都要多。.
What is CNC milling and turning?
CNC milling and turning are the two core machining processes. Turning spins the workpiece against a fixed cutting tool to make round features — shafts, bores, threads — while milling spins the tool against a stationary part to cut flats, pockets, slots, and holes. Most real parts need both, which is why shops quote them together and why mill-turn centers finish both in one setup.
What is mill-turn machining?
Mill-turn machining is machining on a mill-turn center: a lathe with a powered milling head, usually with a second spindle, that turns and mills the same part in a single clamping. The part is never unclamped between operations, so every feature is cut relative to the same datum — that is what protects concentricity and cuts lead time.
What is the difference between CNC milling and turning?
The difference is what moves. In turning, the part rotates and the tool stays put, which is fastest for round features. In milling, the tool rotates and the part stays put, which is best for flats, slots, pockets, and complex 3D shapes. They are not competitors — they are two halves of the same job, and most parts need both.
那么,你的零件需要哪种配置呢?
Milling and turning are not rival processes to pick between — they are partners. Turning gives you fast, precise round features; milling gives you flats, pockets, and holes.
The strategic decision is not which one, but how many setups your part needs, and whether a single mill-turn machine can finish it in one clamping. Get that right and you win on all three fronts buyers care about: tighter tolerances, lower cost, and shorter lead time.
关于作者 陈帕特里克——XY Machining 应用工程师 帕特里克负责审查XY Machining公司美国工程团队设计的薄壁零件,并与车间人员合作,针对夹具和刀具路径进行优化,以确保精密零件的尺寸公差符合要求。为了在报价前对薄壁零件进行压力测试,, 将您的模型发送给我们的团队.


