Quick answer
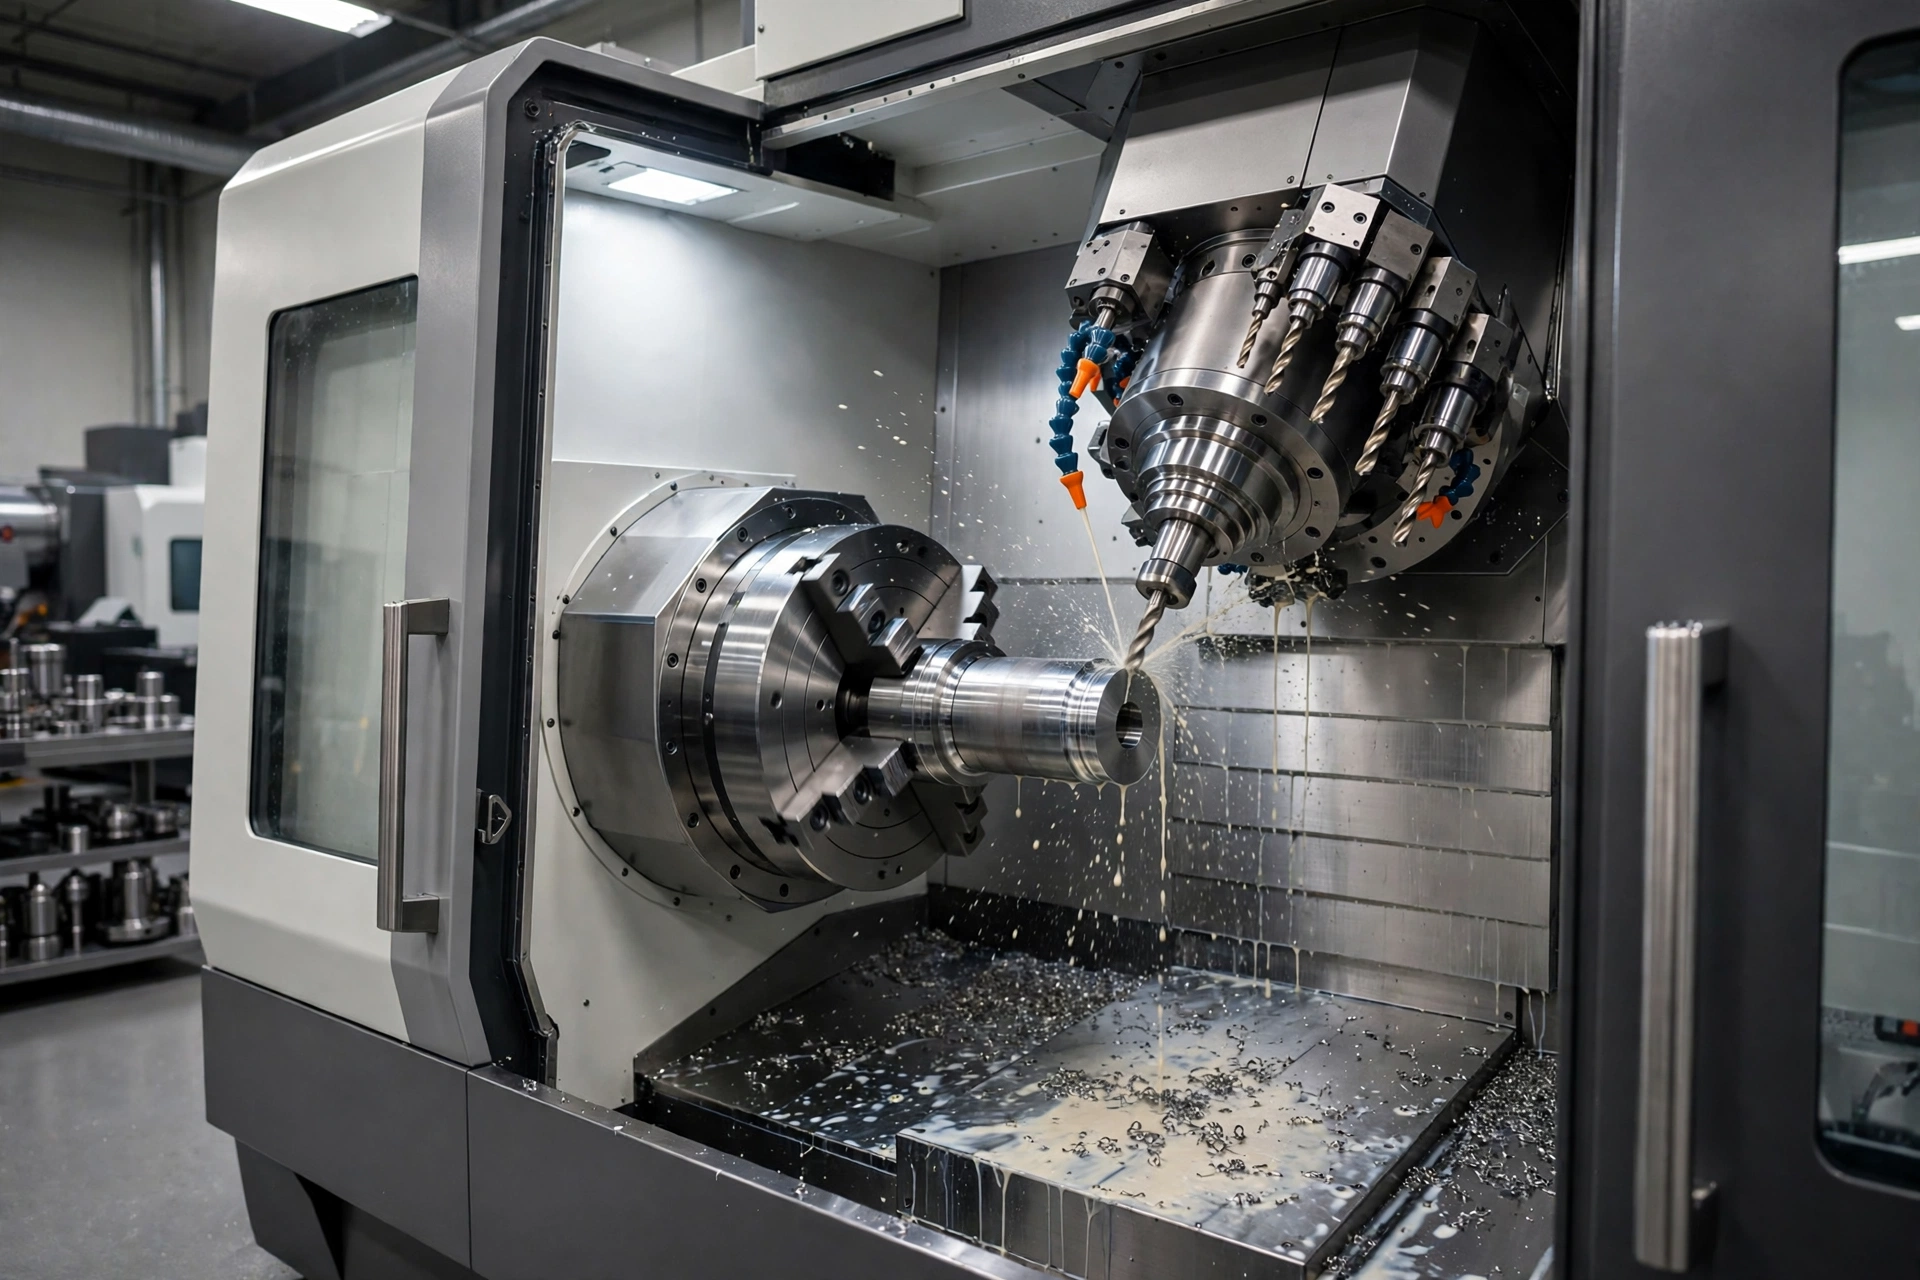
Quick answer: CNC turning spins the workpiece against a stationary cutting tool to make round features fast, while CNC milling holds the part still and spins the tool to cut flats, slots, pockets, and holes. Most real parts need both.
Running them on a single mill-turn machine — instead of moving the part between two separate machines — removes a second setup, protects your tolerances, and typically shaves days off the lead time. That combination is why most precision shops quote milling and turning as one integrated capability rather than two line items.
A bracket that failed inspection
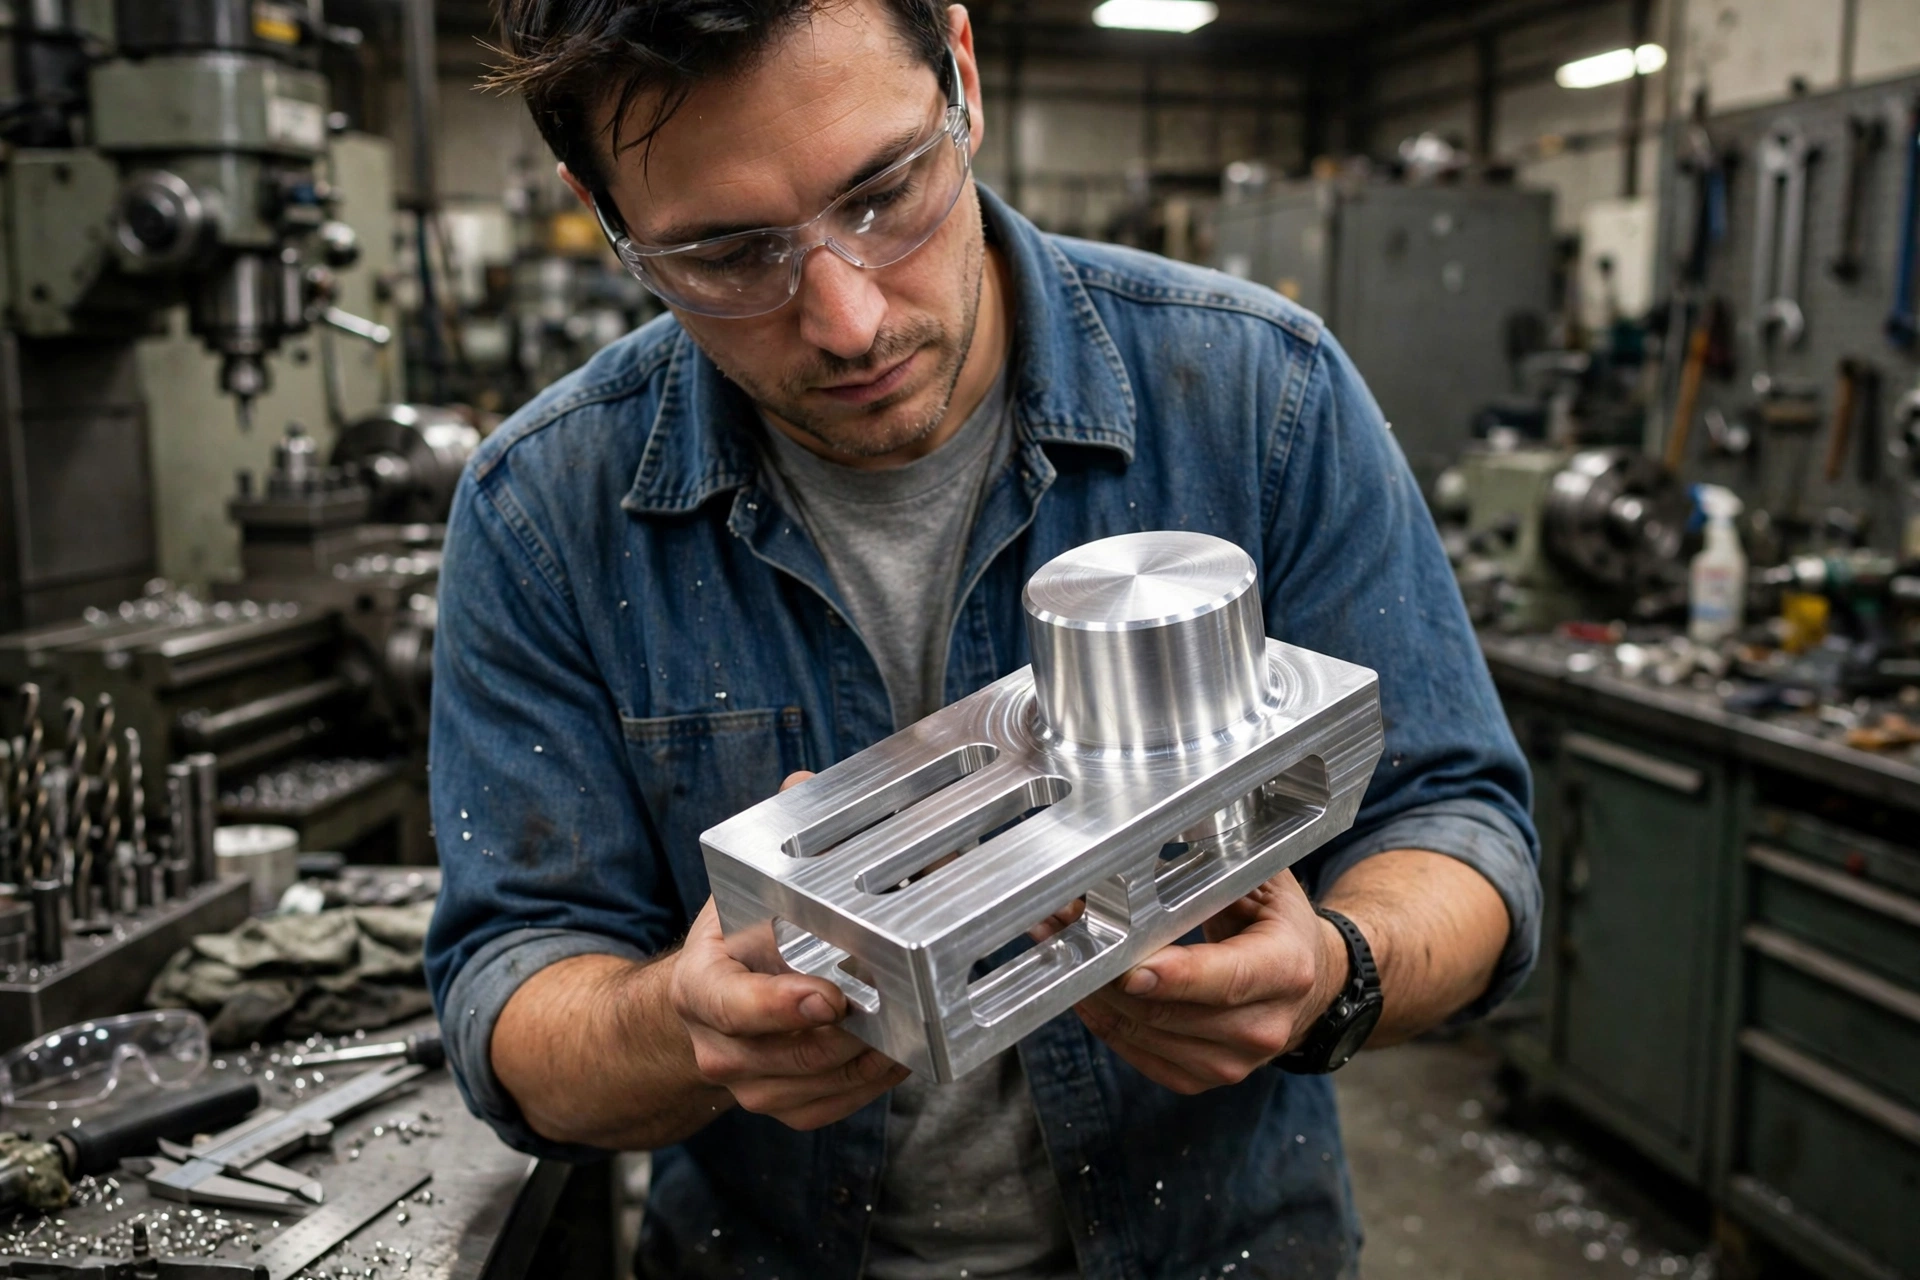
I still remember the first bracket I sent out that needed a turned boss on one face and a milled slot on the other. We machined the turning on a lathe, walked the part across the shop, re-fixtured it on a mill, and lost the concentricity between the two features by four thousandths of an inch. The part failed inspection.
A mill-turn machine would have held both features in one clamping. That lesson is the whole reason this article exists.
Turning vs Milling: the core difference
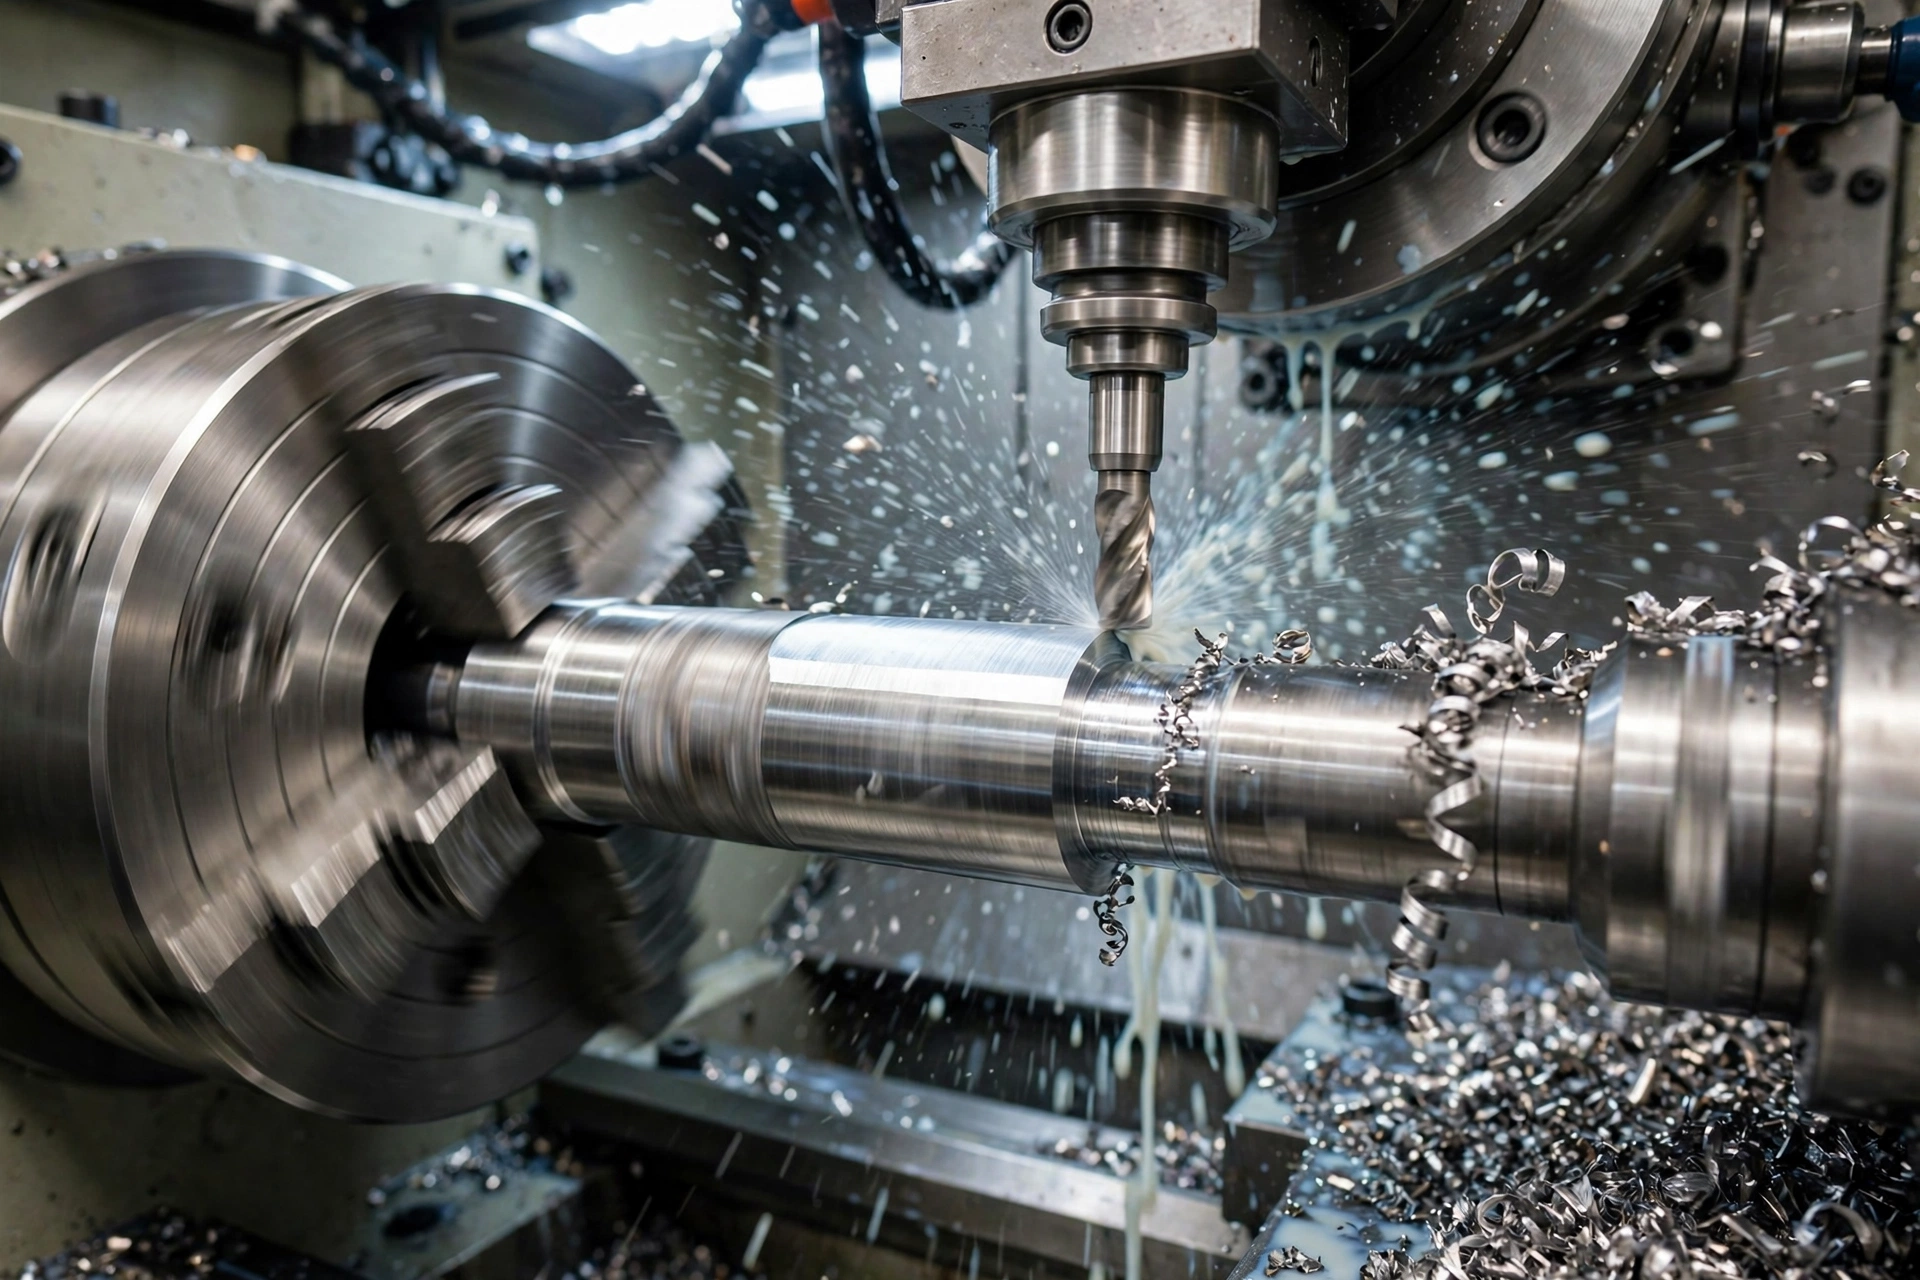
The split is about what moves. In turning, the part rotates and the tool stays put. In milling, the tool rotates and the part stays put (or moves along programmed axes). That single distinction drives everything else — the shapes you can make, the finishes you get, and the cost per part.
| Factor | CNC Turning | CNC Milling |
|---|---|---|
| What rotates | The workpiece | The cutting tool |
| Best for | Cylindrical, round, symmetrical parts | Flat faces, slots, pockets, complex 3D |
| Typical parts | Shafts, bushings, pins, threaded studs | Brackets, housings, plates, manifolds |
| Speed on round features | Very fast | Slow |
| Speed on prismatic features | Poor | Very fast |
| Common axes | 2-axis (X, Z), plus live tooling | 3-axis, up to 5-axis |
| Surface finish on OD | Excellent, mirror-like | Good, may show tool marks |
If you want the deeper head-to-head, we break it down further in our guide on CNC turning vs milling. The short version: they are not competitors. They are two halves of the same job.
Why “milling and turning” is searched as one phrase
People type turning and milling or cnc milling and turning together for a reason. Very few functional components are purely round or purely prismatic. A hydraulic fitting is turned on the outside but needs cross-drilled ports milled into it. A motor shaft is turned to diameter but needs a milled keyway.
When you ask a shop for “milling and turning,” you are really asking a practical question: can you finish my whole part without shipping it somewhere else? That is where mill-turn machining earns its keep.
What a mill-turn machine actually does
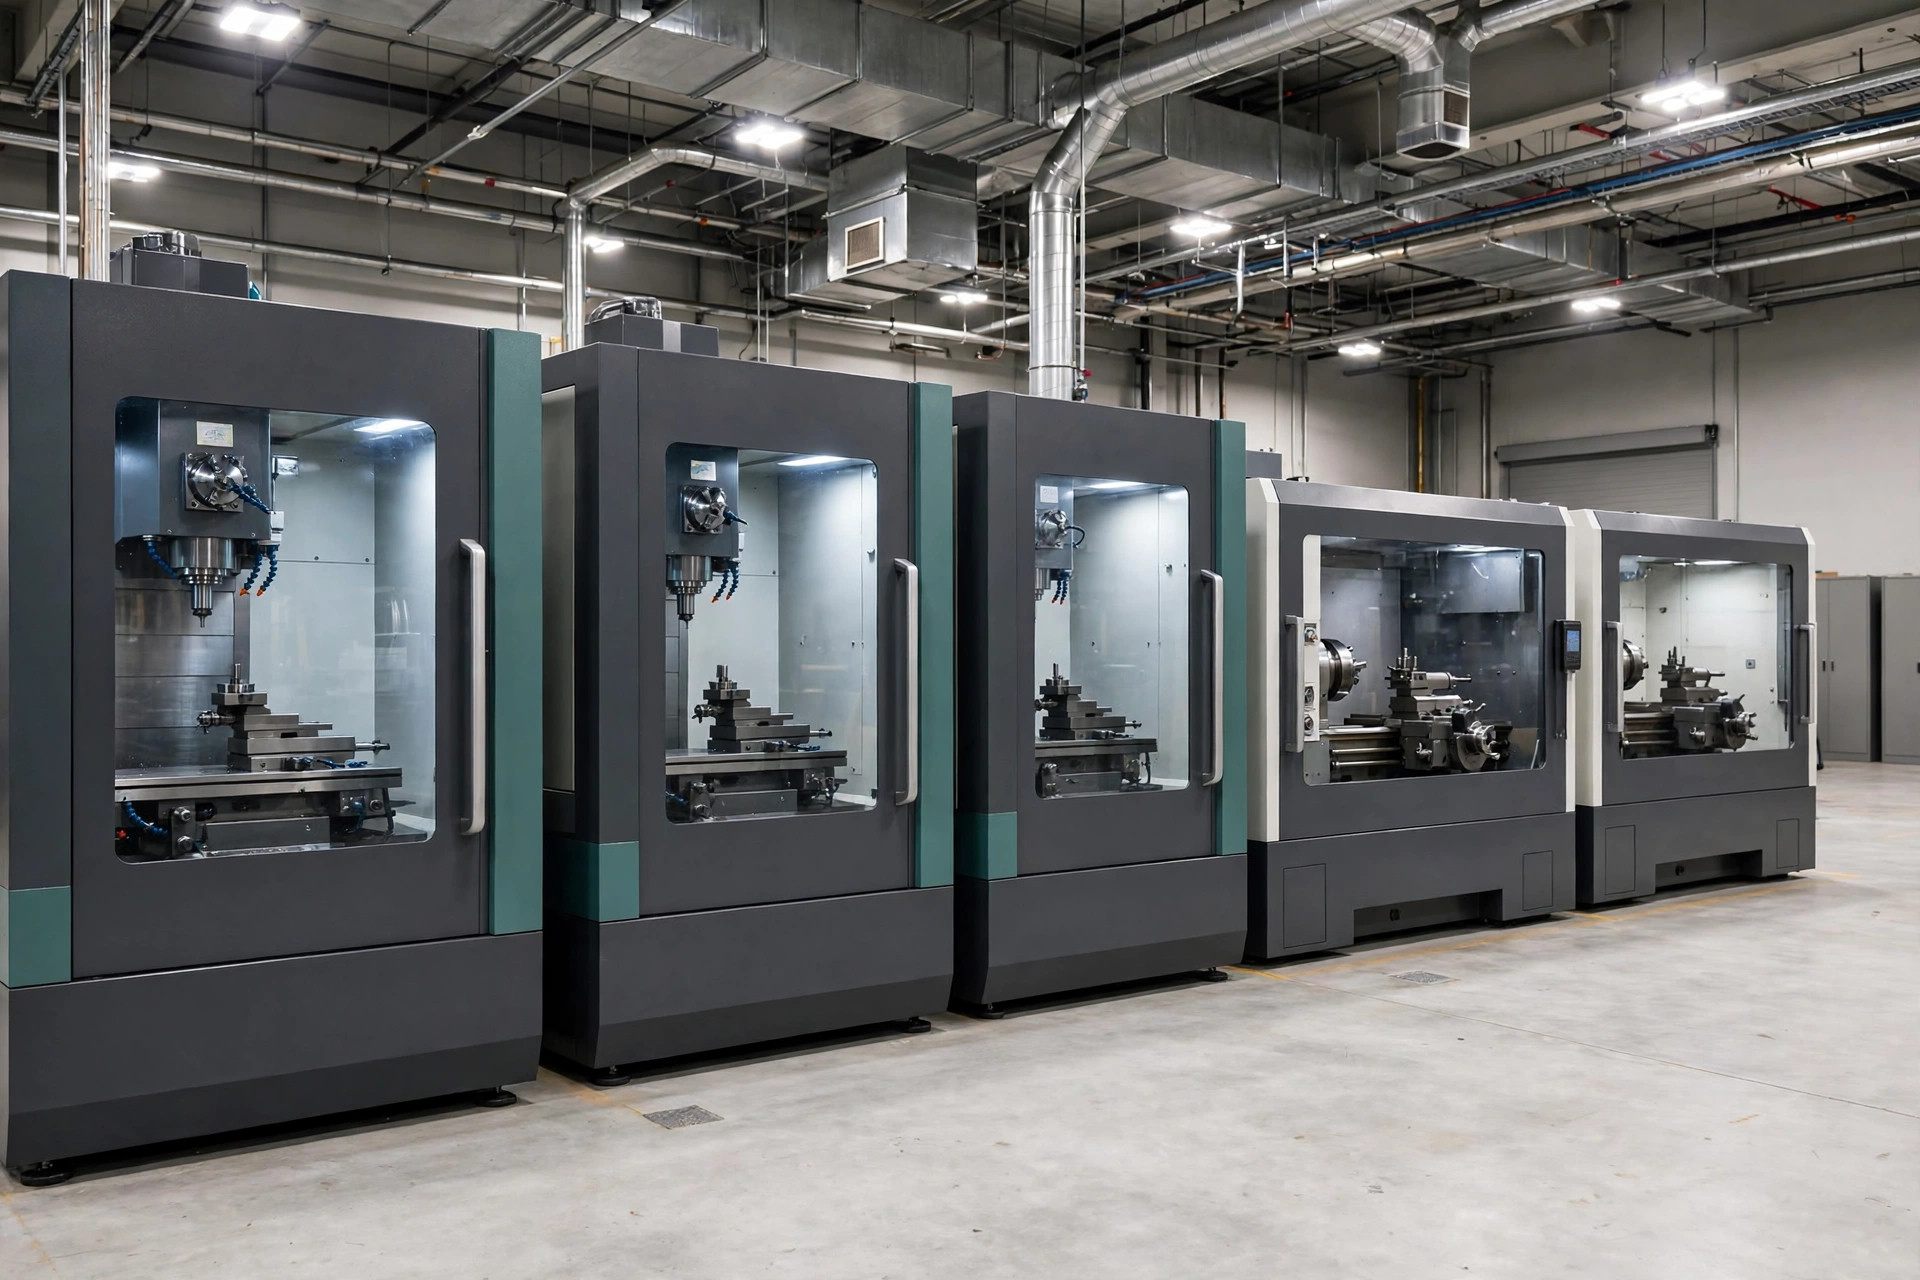
A mill-turn center is a lathe with a powered milling head and, usually, a second spindle. The part rotates for turning operations, then the machine stops the spindle, indexes the part to an exact angle, and drives a live rotating tool to mill flats, drill holes off-center, or cut a keyway — all without unclamping the part.
The benefits stack up quickly:
- One setup, one datum. Every feature is cut relative to the same reference, so concentricity and position error stay tiny.
- No re-fixturing labor. Moving a part between machines is human time, and human time is where cost and mistakes live.
- Shorter lead time. Fewer setups means fewer queue steps between machines.
- Better repeatability at volume. Once the program is proven, part 1 and part 5,000 look identical.
For a precision turning supplier, this is the difference between quoting a 3-day job and a 7-day job on the same drawing.
A realistic cost and lead-time comparison
Below is a representative comparison for a medium-complexity part — say, a threaded aluminum housing with a turned body and four milled side ports — at a quantity of 250. Numbers are illustrative and vary by geometry, material, and shop, but the shape of the difference is consistent with what we see on the floor.
| Approach | Setups | Est. lead time | Relative cost/part | Concentricity risk |
|---|---|---|---|---|
| Separate lathe + separate mill | 2 (re-fixtured) | 6–8 days | Baseline (100%) | Higher |
| Mill-turn (single machine) | 1 | 3–4 days | ~80–90% | Very low |
| Turning only (part redesigned to avoid milling) | 1 | 2–3 days | ~70% | N/A |
The last row is the one buyers forget: sometimes the cheapest move is a small design change. If a milled feature exists only because the original designer defaulted to it, a quick chat with the shop can turn a two-operation part into a one-operation part. This is exactly the kind of design-for-manufacturing thinking that lowers your unit price. We cover more of it in how to reduce CNC machining costs.
When you still want two separate machines
Mill-turn is not always the answer. Dedicated machines can win when:
- Volumes are very high and geometry is simple. A plain turned pin at 100,000 pieces runs cheapest on a fast, dedicated lathe.
- Milling work is heavy and 5-axis. A complex impeller belongs on a full 5-axis machining center, not a lathe with a milling head.
- The turned and milled features have loose tolerances between them. If nothing needs to be concentric, the re-fixturing risk disappears and cost rules the decision.
A good shop tells you which path fits your drawing instead of forcing every job onto one machine.
Materials: how milling and turning behave differently
Material choice changes how each process performs. Free-machining brass and aluminum turn beautifully and mill cleanly. Stainless and titanium turn well but work-harden if the milling feeds are wrong, which is where an experienced operator matters more than the machine’s spec sheet.
| Material | Turning behavior | Milling behavior | Notes |
|---|---|---|---|
| Aluminum 6061 | Excellent | Excellent | The default for prototypes; see 6061 vs 7075 |
| Brass C360 | Outstanding | Very good | Fastest material to machine |
| Stainless 303/304 | Good | Moderate | 303 machines far easier than 304 |
| Titanium Ti-6Al-4V | Moderate | Demanding | Slow feeds, sharp tools, flood coolant |
| Delrin / acetal | Excellent | Excellent | Great for turned insulating parts |
How to brief a shop for a mill-turn job
To get an accurate, fast quote, give the shop:
- A STEP file plus a 2D drawing that calls out the critical dimensions — not every dimension, just the ones that matter for fit and function.
- Tolerances only where you need them. A blanket ±0.001 in on a whole part triples the price for no reason.
- Material and finish clearly stated, including any anodizing or plating.
- Quantity and target date, so the shop can pick the right machine strategy.
That four-item brief is the single biggest lever you control over both cost and lead time.
Frequently asked questions
Is CNC turning cheaper than CNC milling?
For round features, yes — turning removes material far faster than milling because the whole part is spinning. But comparing them in isolation misses the point. The real cost driver is how many setups your part needs. A part that is 90% round and 10% milled is cheapest on a mill-turn machine, because you pay for one setup instead of two. Judge cost by the finished part, not by the individual process.
What is the difference between a mill-turn machine and a lathe with live tooling?
They overlap, and the terms get used loosely. A lathe with live tooling can drive a few rotating tools for light milling and cross-drilling while the part is chucked. A full mill-turn center goes further, usually adding a Y-axis, a second spindle for back-work, and enough milling power to treat the machine almost like a lathe and a machining center fused together. For complex one-setup parts, the full mill-turn center is what you want.
Can one machine really hold tolerance across both turned and milled features?
Yes, and that is precisely why buyers choose it. Because the part never leaves the chuck, every milled hole and flat is referenced to the same turned datum. Concentricity and true-position errors that creep in when you re-fixture on a second machine simply never get introduced. For anything where a milled feature must stay concentric with a turned bore, single-setup machining is the reliable route.
Do I need to design my part specifically for mill-turn?
Not upfront, but a short design review pays off. Send your model to the shop early and ask whether any feature forces an extra operation. Small changes — relocating a port, opening a non-critical tolerance, adding a relief — can collapse a two-op part into a one-op part. That single conversation often saves more money than any material substitution.
What is CNC milling and turning?
CNC milling and turning are the two core machining processes. Turning spins the workpiece against a fixed cutting tool to make round features — shafts, bores, threads — while milling spins the tool against a stationary part to cut flats, pockets, slots, and holes. Most real parts need both, which is why shops quote them together and why mill-turn centers finish both in one setup.
What is mill-turn machining?
Mill-turn machining is machining on a mill-turn center: a lathe with a powered milling head, usually with a second spindle, that turns and mills the same part in a single clamping. The part is never unclamped between operations, so every feature is cut relative to the same datum — that is what protects concentricity and cuts lead time.
What is the difference between CNC milling and turning?
The difference is what moves. In turning, the part rotates and the tool stays put, which is fastest for round features. In milling, the tool rotates and the part stays put, which is best for flats, slots, pockets, and complex 3D shapes. They are not competitors — they are two halves of the same job, and most parts need both.
So which setup does your part need?
Milling and turning are not rival processes to pick between — they are partners. Turning gives you fast, precise round features; milling gives you flats, pockets, and holes.
The strategic decision is not which one, but how many setups your part needs, and whether a single mill-turn machine can finish it in one clamping. Get that right and you win on all three fronts buyers care about: tighter tolerances, lower cost, and shorter lead time.
About the author Patrick Chen — Applications Engineer, XY Machining Patrick reviews thin-wall designs for US engineering teams at XY Machining and works with the shop floor on the fixturing and toolpaths that keep delicate parts in tolerance. To pressure-test a thin-wall part before quoting, send your model to our team.