
Quick answer
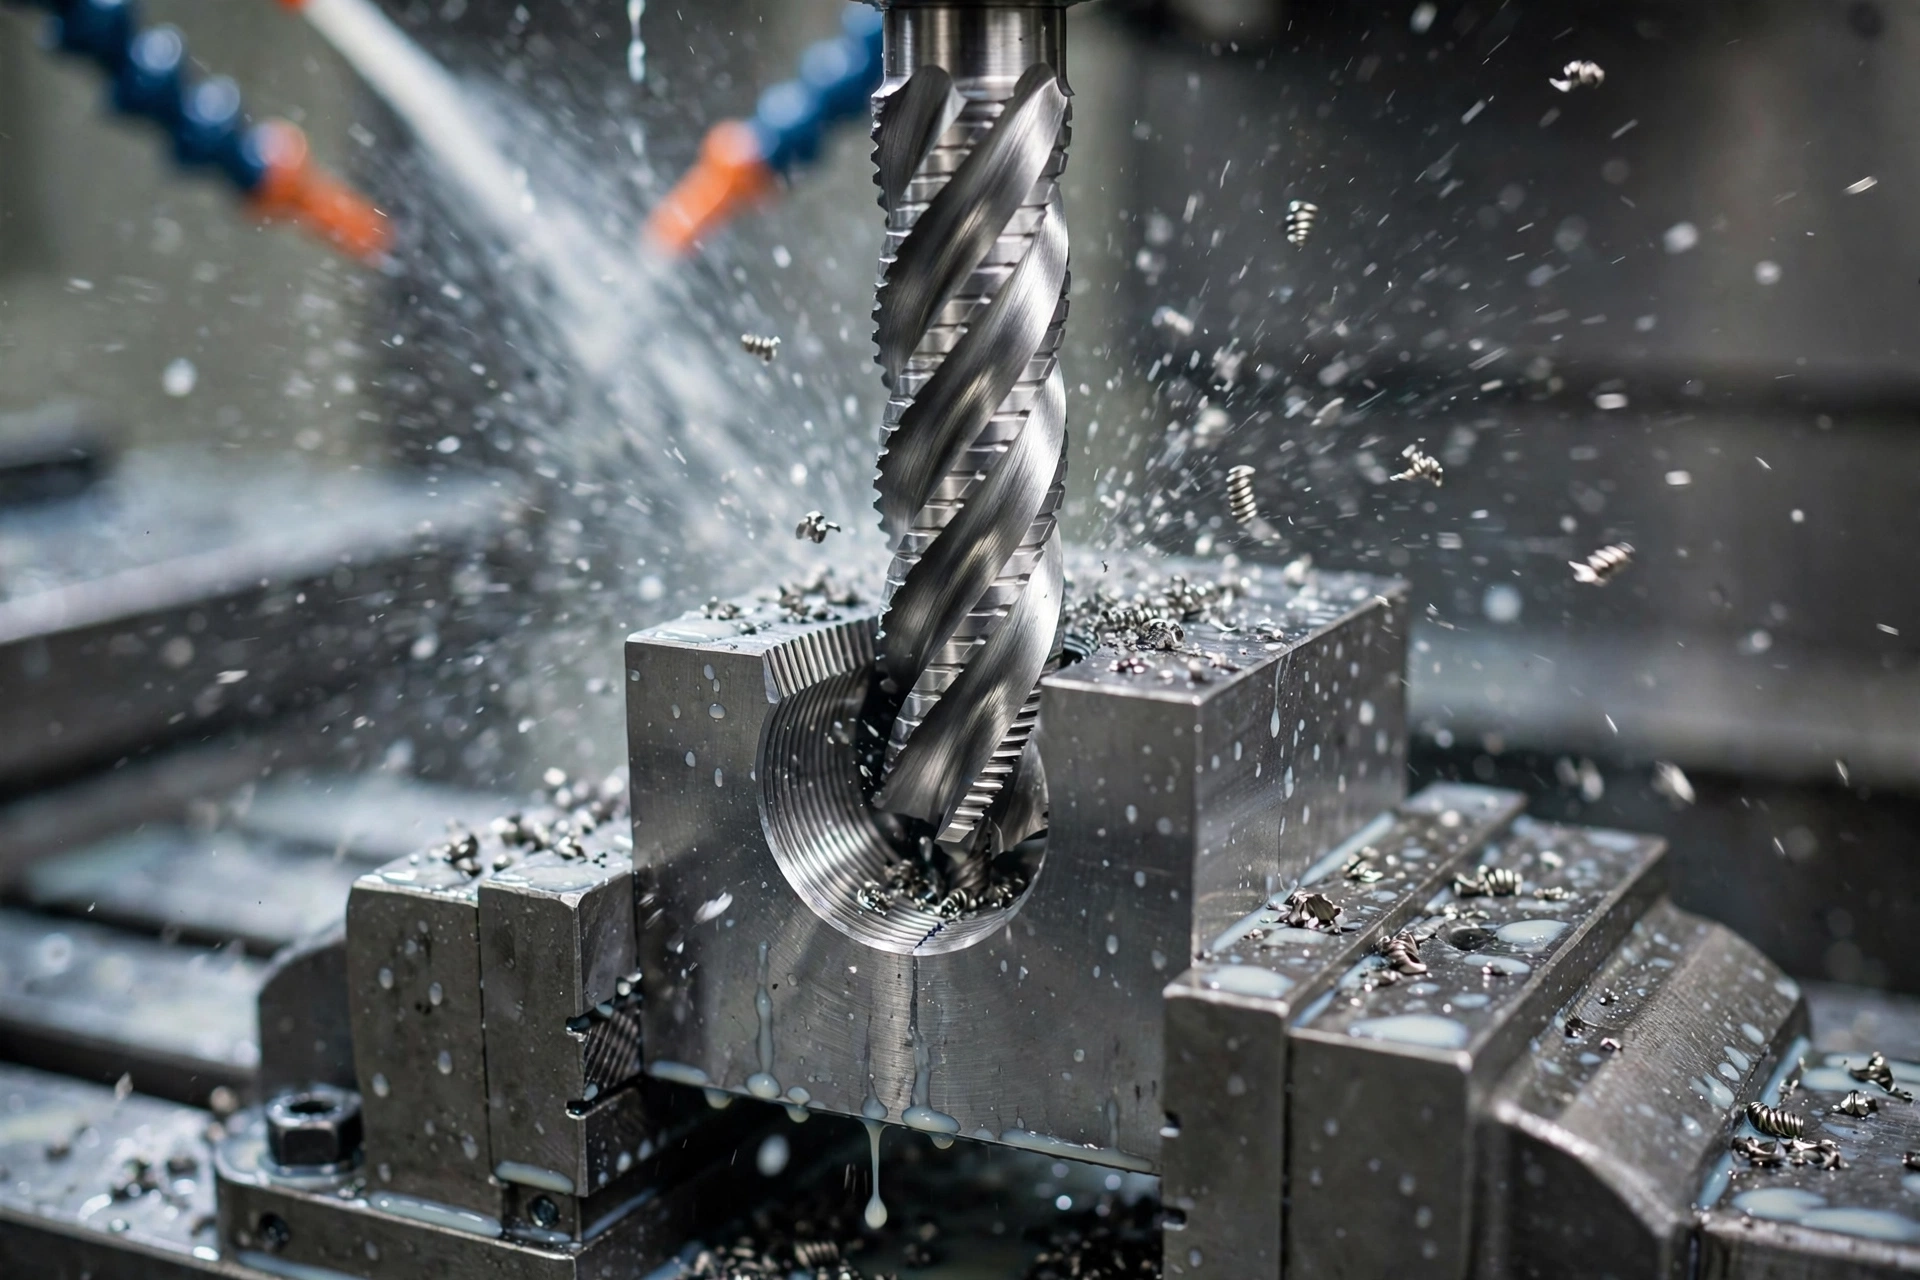
Thread milling vs tapping comes down to speed against control. Thread milling is slower per hole, but one cutter covers many sizes, cutting forces stay low, and the thread can be milled all the way to the bottom of a blind hole.
Tapping is faster and cheaper for small, standard threads in high-volume production, because the tap cuts the whole thread in one pass. For large or custom threads, tough materials, and blind holes, thread milling is the better choice.
Two ways to cut the same thread
Every CNC machined part with an internal thread was either tapped or thread-milled. Both operations produce the same output — a threaded hole — but they work by entirely different mechanisms, and the choice between them has real consequences for tool breakage risk, tolerance, material compatibility, and cost.
Both methods are available as part of our CNC machining services, and threading often pairs with the process choices in our CNC turning vs milling guide.
How tapping works
Tapping drives a dedicated tap directly into a pre-drilled hole in a single axial plunge. The tap geometry matches the thread form exactly, so the operation is fast and requires minimal programming. For high volumes of standard threads in ductile materials, tapping is hard to beat on speed and economy.
A tap is a hardened cutting tool ground with flutes and a thread form that matches the target internal thread exactly. It is mounted in the spindle and driven axially into a pre-drilled hole at a feed rate synchronized to its pitch — this is rigid tapping, the standard mode on modern CNC machining centers.
Rigid tapping and cycle time
In rigid tapping, spindle speed and axial feed are electronically synchronized so the tap advances exactly one pitch per revolution, then reverses and extracts in one continuous cycle.
For a part with thirty M5 holes in 6061 aluminum, tapping is extremely productive — cycle time per hole is typically one to three seconds for standard sizes. One tap per thread size and pitch means five different M-size threads require five taps, consuming five tool magazine slots. In high-volume dedicated cells, this is negligible. In job-shop work with complex parts running mixed thread specifications, tool magazine management becomes a real consideration.
Chip management
Chip management is more challenging in tapping than in thread milling, especially in blind holes. Flutes must carry chips out of the hole as the tap advances. In materials that produce long, stringy chips — 304 stainless, titanium, some nickel alloys — chips pack around the flutes and increase binding and breakage risk. Spiral-flute (gun-tap) designs lift chips axially out of blind holes and reduce but do not eliminate this risk.
When a tap breaks
Its vulnerability is tool breakage: a broken tap inside a blind hole in a hard material is often unrecoverable and can scrap an otherwise complete part.
When a tap breaks — particularly in a hardened material in a blind hole — it is typically hardened HSS or carbide and cannot be drilled out. EDM (electrical discharge machining) is often the only reliable removal method, which is expensive and time-consuming. Depending on part complexity and value, the result may be scrap.
How thread milling works
Thread milling uses a smaller rotating cutter that follows a helical CNC toolpath — circling the hole in X and Y while advancing in Z — to generate the thread form over several passes. The cutter does not match the thread diameter, which means one tool covers a range of thread sizes at the same pitch, and fit can be fine-tuned by adjusting the toolpath radius.
Thread milling is slower and requires more sophisticated programming, but it is safer, more flexible, and better suited to hard materials, large threads, blind holes requiring clean bottom engagement, and expensive parts where breakage risk cannot be accepted.
The cutter and the toolpath
A thread mill is a multi-tooth rotating cutter, typically solid carbide with a wear-resistant coating, that the CNC machine moves along a helical path — interpolating simultaneously in X, Y, and Z — to generate the thread form. The cutter’s tooth geometry matches the thread profile, and the toolpath diameter determines the thread size.
Because the path diameter controls the size rather than the tool body, a single thread mill can produce multiple thread sizes sharing the same pitch by adjusting the programmed radius.
Fit control and safety
Thread milling also provides control over thread fit that tapping does not. By shifting the programmed toolpath radius by a few microns, the operator can tighten or loosen the fit class without changing tools. This is particularly valuable for precision instrument housings, hydraulic fittings, and fluid connectors where the fit class must be verified and adjusted part-to-part.
The safety advantage is significant. The thread mill cutter is smaller than the finished thread diameter. If it breaks, the fragment can fall free of the thread or be extracted with a magnet or forceps. The part is typically recoverable — a sharp contrast to a broken tap in a blind hole.
The speed trade-off
Thread milling is slower: multiple helical passes per hole rather than one axial plunge. It requires a CNC machining center capable of simultaneous three-axis interpolation and a CAM system or thread-milling canned cycles. For very high volumes of standard threads in ductile materials, the per-hole time disadvantage adds up and tapping is more economical.
Thread milling is also the tool of choice on a mill-turn center, where the same setup turns and mills the part — one cutter covers the sizes that would need a whole set of taps.
Thread milling vs tapping: comparison table
Thread milling vs tapping comes down to brute-force speed against flexibility and control. The right choice depends on thread size, material, hole type, and the accuracy your part needs.
| Factor | Tapping | Thread Milling |
|---|---|---|
| Cycle time per hole | Fastest — single plunge | Slower — helical multi-pass |
| Programming complexity | Simple rigid tap cycle | Helical interpolation, CAM required |
| Tool per size/pitch | One tap per size and pitch | One mill covers many sizes (same pitch) |
| Breakage risk | Moderate–high; scraps part | Low; cutter falls free |
| Best materials | Aluminum, mild steel, brass | Titanium, stainless, hardened steels |
| Blind hole performance | Chip-packing risk; runout zone at bottom | Clean bottom threads; chips exit outward |
| Thread quality and fit | Good; fixed by tap geometry | Excellent; adjustable by toolpath offset |
| Right- and left-hand | Separate tap required | Same mill, reverse toolpath direction |
| External threads | Not applicable | Possible with climb-cut helical path |
| Best volume | High volume, standard threads | Low–medium, precision or unusual threads |
If your priority is speed, tapping often wins. If your priority is precision and flexibility, thread milling is the better choice.
Material guide: when to tap and when to thread mill
Aluminum alloys
Aluminum alloys — 6061, 7075, cast grades — are the natural home of tapping. The material is ductile, produces manageable chips, and its relatively low yield strength keeps tapping forces and wear modest. Standard HSS or cobalt taps produce thousands of holes before wearing out.
Thread milling in aluminum is possible and preferred for threads M20 and above or blind holes needing clean bottom engagement, but for M3 through M16 at volume, tapping is more economical.
Stainless steels
Stainless steels — 304, 316, 17-4 PH — work-harden rapidly, generate long stringy chips, and are abrasive to cutting edges. Tapping in stainless is possible with sharp spiral-flute taps, appropriate cutting fluid, and careful synchronization, but wear is faster and breakage risk is higher than in aluminum.
Thread milling is often the better choice for M12 and above in stainless: the cutter engages a smaller chip cross-section per pass, work-hardening is distributed across multiple light cuts, and breakage risk is substantially reduced.
Titanium alloys
Titanium alloys — 6Al-4V in particular — concentrate heat at the cutting edge due to low thermal conductivity, accelerating wear and increasing galling risk. Tapping titanium requires carbide taps, high-pressure through-spindle coolant, and conservative speeds — and breakage remains a real risk. Thread milling in titanium with solid carbide cutters and appropriate coatings provides better heat management and far lower breakage risk. For structural aerospace threads in titanium, thread milling is the industry standard.
Hardened steels
Hardened steels above approximately 40 HRC are generally not tapped — the breakage risk is prohibitive. Thread milling with carbide cutters designed for hard material can produce threads up to approximately 65 HRC, though tool wear is high and feed rates must be conservative.
Blind holes: thread milling’s key advantage
A blind hole — one that does not pass through the workpiece — creates specific challenges for both methods. With a standard taper tap, the chamfer geometry prevents full thread engagement for three to five pitches from the bottom of the hole. A bottoming tap reduces this to one to two pitches, but chip packing at the bottom increases breakage risk.
If full thread engagement close to the blind end is a structural requirement, note it on the drawing so your machinist can select the right tap type or recommend thread milling.
Threads all the way to the bottom
Thread milling handles blind holes more cleanly. The cutter begins the helical path at the bottom of the thread depth and spirals upward toward the hole entrance, so chips move toward the open end rather than packing at the bottom.
The cutter can engage the thread form within one pitch of the blind end, providing nearly full engagement across the specified thread depth. For blind holes where thread depth is limited and full engagement is structurally required, thread milling is typically the correct choice.

Choosing the right method: a decision framework
Default to tapping
Default to tapping when: the material is aluminum, mild steel, or brass; the thread is a standard size and pitch; the volume is sufficient to justify dedicated tapping cycles; and the hole depth and part value do not create unacceptable breakage risk. For most high-volume work in ductile materials, tapping is the economical default.
Choose thread milling
Choose thread milling when any of the following apply: the material is stainless steel, titanium, or hardened steel; the thread is M20 or larger, an unusual pitch, or left-hand; the hole is blind and requires clean bottom thread engagement; the fit class is tight and per-part adjustment is needed; or the part value is high enough that a broken tap scrapping it would be a significant loss.
Use both on the same part
Use both on the same part where it makes sense: tap the twenty M5 holes in the aluminum bracket; thread mill the two M30 features in the stainless insert. Specifying a single method for an entire part often leaves cost or quality on the table.
Frequently asked questions
Is thread milling always better than tapping?
Not always. Thread milling is more flexible, safer in hard materials, and provides adjustable fit — but it is slower and requires more capable machine and programming infrastructure. Tapping is faster and simpler for standard threads in ductile materials at volume. The best method depends on material, thread size and type, hole geometry, part value, and production volume.
When should I use thread milling instead of tapping?
For hard materials — titanium, stainless steel, hardened steels — large or unusual threads, blind holes needing clean bottom engagement, tight fit tolerances where adjustment is needed, and expensive parts where a broken tap would be a costly scrapping event.
Why is tapping faster than thread milling?
A tap cuts the complete thread in a single axial plunge, typically in one to three seconds per hole. Thread milling requires the machine to complete a full helical pass — circling the hole while advancing axially — over multiple passes. For high volumes of standard threads, the per-hole time advantage of tapping is significant.
What happens if a tap breaks inside a blind hole?
A broken tap in a blind hole is one of the hardest recovery situations in CNC machining. Taps are hardened HSS or carbide and cannot be drilled out. EDM (electrical discharge machining) is often the only reliable removal method, expensive and time-consuming, and the part may be scrapped. Thread milling significantly reduces this risk: the cutter is smaller than the hole and, if it breaks, the fragment typically falls free, leaving the part recoverable.
Can thread milling produce left-hand threads?
Yes. Thread milling produces left-hand threads by reversing the direction of the helical toolpath — no change in tool or tool holder is needed. Tapping requires a separate left-hand tap for each left-hand thread size, to be run with spindle rotation reversed.
What is thread milling?
Thread milling is a CNC process that cuts a thread with a rotating cutter moving in a helical toolpath. The cutter advances in small increments, so cutting forces stay manageable, and the same cutter can produce different thread diameters and pitches by changing the toolpath.
What is a thread mill?
A thread mill is a rotating cutting tool with multiple teeth that cuts internal threads by helical interpolation. Unlike a tap, which needs a dedicated tool for every thread size, one thread mill can cut several sizes and pitches.
What are the downsides of thread milling?
Thread milling is slower per hole than tapping, costs more up front, and needs CNC programming expertise to set up the helical toolpath. For small standard threads in high volume, those costs are hard to justify — which is why tapping still wins there.


